
Manufacturing Compliance: How to Build an Audit-Ready Traceability System
Manufacturing compliance is often discussed as a documentation issue. In practice, the real test is much tougher: can a factory show what happened to a specific product, material lot, batch, or process step when an auditor, customer, regulator, or internal investigation asks for evidence?
A procedure may state that operators verify cleaning, measure batch ingredients, inspect coating thickness, or apply a serial number. An audit-ready traceability system proves that those controls actually occurred, identifies who performed them, connects them to the relevant equipment and materials, and preserves the result in a form that cannot be casually reconstructed after the fact.
That distinction matters in nearly every advanced manufacturing environment. A missed material-lot link can turn a limited supplier issue into a broad recall review. An unreadable inkjet code can leave finished goods impossible to isolate. A vacuum alarm without a corresponding production record may make it difficult to determine whether sensitive product was exposed to an out-of-control condition. The primary machine may make the part, but many compliance failures begin in the supporting processes around it.
Traceability Is a Chain of Evidence, Not a Collection of Records
A useful traceability model follows the product in both directions. Forward traceability answers: “Where did this material lot or nonconforming batch go?” Backward traceability answers: “What materials, settings, people, equipment, and inspections contributed to this finished unit?” Both are needed. A system that can find a finished product but cannot identify its incoming material is only half-built.
For many plants, the minimum evidence chain includes incoming material identification, receiving status, work order or batch number, process route, machine or station identity, relevant process parameters, operator or automated-system approval, in-process inspection, final release status, packaging identity, and shipment records. Not every product requires the same depth. A commodity part and a safety-critical assembly should not be treated as if their risk is identical. The depth of the record should follow the consequences of failure, customer obligations, applicable regulations, and contractual requirements.
This is where teams often make an expensive mistake: they collect too much low-value information while missing the few fields that establish cause and containment. Recording every screen view an operator sees is not necessarily useful. Recording the actual recipe version, scale verification status, vacuum level trend where it is process-critical, or cure profile linked to a coating batch may be far more valuable.
Start with the Questions an Auditor Will Actually Ask
Before choosing software, labels, scanners, or marking technology, map the questions the business must answer under pressure. A good exercise is to select one shipped product identifier and ask the team to retrieve its full history. Then select one incoming material lot and ask where it was used. If either exercise depends on personal memory, loose spreadsheets, or searching through unlinked paper files, the traceability system has a weak point.
The evidence required will vary by process, but the logic remains consistent:
The goal is not to make every event complicated. It is to make critical events unambiguous. If an operator can select the wrong material from a list of nearly identical codes, or if a machine can run an obsolete program without warning, a complete-looking database will not protect the operation.
Define the Traceability Unit Before Designing the Data Flow
One of the earliest decisions is the traceability unit: the smallest quantity that must be individually identified and controlled. Depending on the product, this may be a pallet, container, production batch, reel, tray, component, assembly, or serialized finished unit.
Overly broad units reduce containment precision. If one questionable component lot is mixed across several days of production without a reliable consumption record, the resulting investigation may include far more inventory than necessary. At the other extreme, serializing every low-risk item can add cost, scanning burden, and opportunities for data-entry errors without improving risk control. The right choice is a risk decision, not a default preference for “more data.”
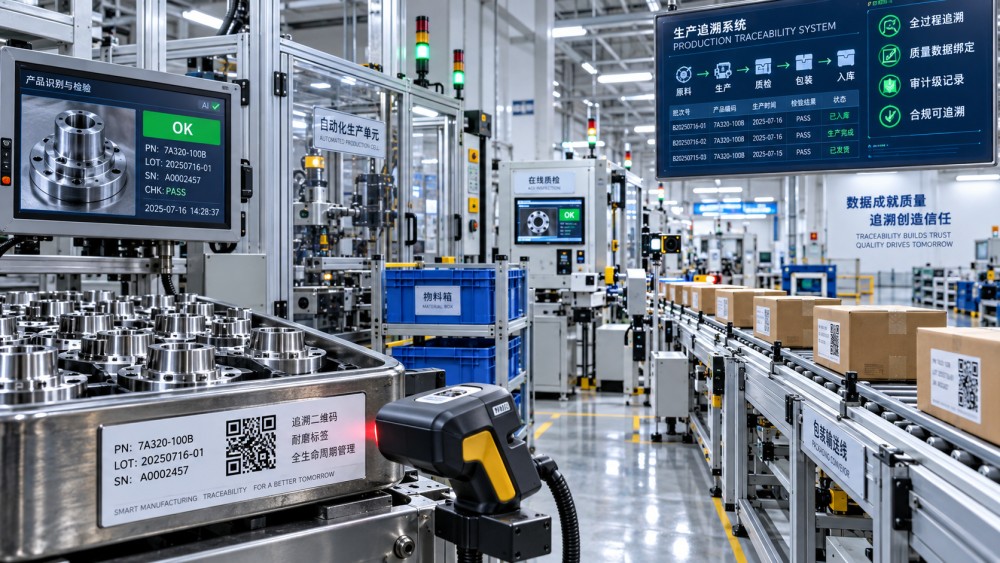
The identifier itself also needs practical scrutiny. It must survive the real production environment: cleaning chemicals, heat, abrasion, outdoor storage, coating, packaging friction, or subsequent assembly. Laser marking may be appropriate where permanence and legibility are essential, but the mark must be validated on the actual substrate and surface condition. Inkjet coding can be effective for cartons, packaging, and high-speed lines, yet print contrast, adhesion, and code verification require routine attention. A code that exists but cannot be read reliably is not a traceability control.
Connect Auxiliary Systems to the Product Record
Manufacturers frequently focus their records on the main production machine while treating supporting equipment as background infrastructure. That is rarely sufficient when those systems influence product conformity.
Consider ultrasonic cleaning before precision assembly or coating. The cleaning cycle may be a prerequisite for adhesion, sealing, or contamination control. An audit trail may need to show the load identity, cleaning program, time, solution-management checks where applicable, and release decision. It does not always require recording every available machine signal; it does require capturing the controls that demonstrate the approved process was followed.
The same principle applies to industrial weighing and batching. In food, pharmaceutical, chemical, and lithium battery applications, the identity and quantity of ingredients can be central to the batch record. A scale reading alone may not be enough if the system cannot prove which material was weighed, against which recipe revision, and whether the measuring equipment was in an acceptable status under the site’s calibration program.
Vacuum systems deserve similar attention in processes such as packaging, degassing, coating, freeze-drying, and semiconductor-related production. If vacuum stability is process-critical, the record should make abnormal conditions visible and link them to the product or batch affected. Simply retaining maintenance logs for the pump does not establish that a particular production run remained within its approved conditions.
Surface treatment and electrostatic coating create another common blind spot. Quality teams may retain final visual inspection results but lose the connection to pretreatment, powder or liquid material lot, application conditions, cure program, and coating-thickness measurements. The exact evidence depends on the product specification and local requirements, but the compliance logic is clear: final appearance cannot always explain long-term corrosion resistance or adhesion performance.
Build for Exceptions, Not Just Normal Production
A traceability system looks impressive when every process runs normally. Audits and investigations usually focus on the opposite condition: an interrupted scan, a failed inspection, a rework loop, a substituted material, a machine alarm, a label reprint, or a manual override.
These events need controlled paths. A reworked product should retain its original identity and show why rework occurred, what was done, and who authorized the disposition. A replacement label should not quietly create a second identity for the same item. Material substitution should require a documented approval route rather than an informal decision made at the line because the approved lot was unavailable.
Electronic records are often preferable for speed and retrieval, but digitization alone is not control. Access rights, audit trails, time synchronization, revision management, backup arrangements, and data retention rules all matter. If operators can overwrite a measured value without preserving the original entry and reason for change, the system may be convenient but difficult to defend. Paper records have their own weaknesses, particularly delayed completion and illegible handwriting, yet a hybrid system can work if handoffs are defined and records are reconciled promptly.
Make the System Verifiable Through Routine Trace Exercises
The most reliable way to expose weak links is to test the system before a customer or regulator does. Periodic trace exercises should begin with realistic samples: a completed shipment, a quarantined raw-material lot, an inspection failure, or a production window affected by an equipment deviation. The team should measure whether it can identify affected stock, work in progress, finished goods, and relevant records within the timeframe expected by its own procedures and customer commitments.
Do not grade the exercise only on speed. Review whether the result is complete and defensible. Were all material lots included? Was rework visible? Did the batch record show the approved recipe revision? Could the inspection record be tied to the same product identity? Did the system identify potentially affected goods that had already been shipped?
This review often reveals mundane but consequential problems: barcode labels placed where scanners cannot read them after packing, duplicate lot numbering across sites, operators sharing logins, disconnected maintenance and quality systems, or a spreadsheet maintained by one knowledgeable person. Those are not software problems alone. They are process-design problems.
Standards Provide Direction, but Site-Level Discipline Provides Evidence
Quality management frameworks such as ISO 9001 emphasize controlled processes, documented information, identification, and traceability where necessary for product conformity. Sector-specific requirements can be more prescriptive, particularly in regulated or safety-sensitive supply chains. However, certification to a management-system standard does not automatically mean that every traceability path is complete. Auditors still examine how the written system operates on the shop floor.
The practical question is always the same: can the organization demonstrate control using objective evidence? That evidence should be proportionate, linked, retrievable, and understood by the people doing the work. The best system is rarely the one with the most dashboards. It is the one that allows a quality team to investigate a specific product without guessing which records matter.
For manufacturers evaluating auxiliary equipment, traceability should therefore be part of technical selection from the start. Ask how a laser marker manages serialized data, how a batching system records recipe revisions and actual weights, how a vacuum controller exports alarms, or how cleaning and coating equipment can associate process status with a load or work order. These details can determine whether a production line is merely automated or genuinely audit-ready.
A durable manufacturing compliance program does not depend on finding the right document during an audit. It creates the evidence as work happens, protects the links between records, and tests those links often enough that a recall or inspection does not become the first real trial of the system.