
Vibration can make a correctly calibrated weighing system report the wrong mass during production. The problem is not always an visibly unstable display: a reading may look steady while filtering delays the result, mechanical connections introduce bias, or the controller accepts a measurement before the assembly has settled. For high precision industrial weighing systems, accuracy must therefore be assessed with surrounding equipment running and within the time available for the weighing operation.
A useful evaluation separates three questions: how vibration reaches the weighing assembly, how the measurement electronics respond, and whether the resulting error affects the process. Improving only one of these can leave the underlying problem unresolved.
Why vibration changes the measured weight
A load cell responds to force. The weighing instrument converts that force into a mass indication using calibration established under defined conditions. When the supported assembly accelerates vertically, the force acting on its supports changes even though the amount of material remains constant.
For a simplified rigid assembly moving vertically, the support force follows F = m(g + a), where m is the supported mass, g is gravitational acceleration, and a is vertical acceleration. The instrument cannot inherently distinguish the additional inertial force from a change in material weight. Real installations are more complicated because frames flex, loads move, and individual supports may experience different forces.
This explains why small visible movements can still matter. Acceleration depends on both displacement and frequency; a movement that is difficult to see can disturb a sensitive measurement. Assessing vibration by touching the platform or watching the floor provides little evidence about weighing accuracy.
The supported mass also matters. A hopper weighing a small ingredient addition may carry a much larger vessel tare. Vibration acts on the moving assembly, including the vessel, while the process tolerance applies to the ingredient dose. Subtracting tare removes its static indication; it does not remove the vessel’s contribution to dynamic forces.
Horizontal motion can affect the result through rocking, side loading, frame distortion, or imperfect load introduction. In a vessel supported by several load cells, movement can redistribute forces between supports. An ideal summation may cancel some redistribution, but actual mounts, structural flexibility, and external restraints can prevent complete cancellation.
Follow the mechanical path before changing settings
Conveyors, mixers, pumps, fans, and nearby machine movements can transmit vibration through floors, platforms, shared frames, and pipework. Equipment mounted directly on a weigh vessel creates another path. An agitator, for example, can introduce periodic forces into the same structure that supports the load cells.
The source need not be the largest machine nearby. A smaller pump connected through rigid piping may influence a weigh tank more strongly than a larger machine on a separate foundation. The relevant issue is how effectively the disturbance reaches the measurement assembly.
Inspect every connection crossing the boundary between the weighed structure and its surroundings. Inlet pipes, discharge connections, ventilation ducts, electrical conduits, and cable bundles can transmit vibration or carry part of the load. Flexible connections help only when their geometry and operating condition allow movement. A flexible hose installed under tension can still exert significant force.
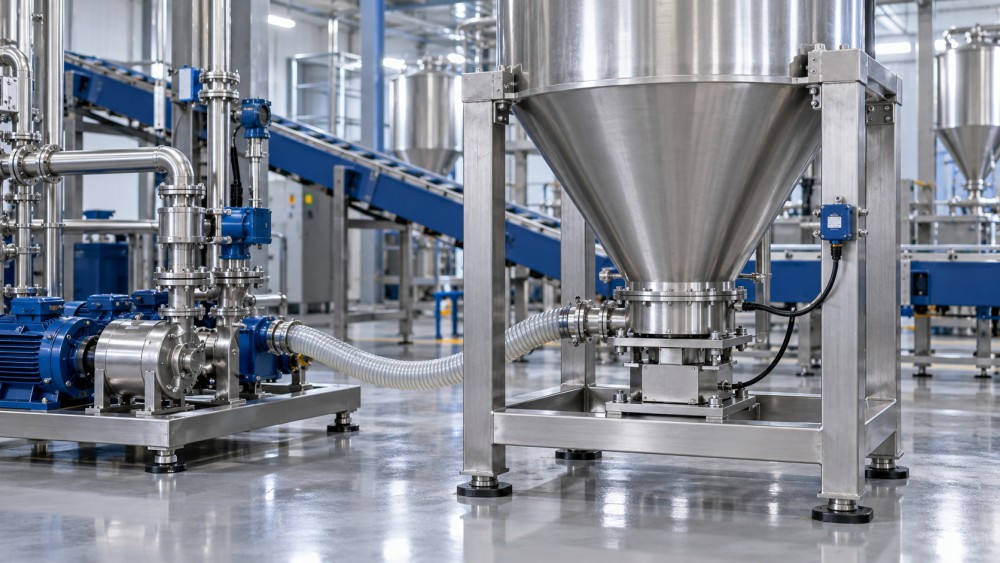
Resonance can magnify these effects. A weighing frame, vessel, mounting assembly, or isolated platform has natural frequencies determined by its mass and stiffness. When an excitation frequency approaches one of them, the assembly may respond strongly. Changes in vessel fill level can shift its dynamic behavior, so satisfactory performance with an empty hopper does not establish satisfactory performance throughout production.
Product movement adds another disturbance. Falling material transfers momentum to a hopper, liquids can slosh, and powder can settle unevenly after filling. These forces are part of the weighing cycle even when nearby machinery is quiet. The installation must accommodate both environmental vibration and disturbances generated by the process itself.
A stable display can conceal a poor measurement
Digital filtering suppresses selected signal variations, making the indication easier to read and helping the controller obtain a usable measurement. It is valuable when properly matched to the disturbance and process timing. However, a filter changes the information available to the controller; it does not correct the mechanical load path.
Averaging and low-pass filtering generally trade responsiveness for reduced fluctuation. During filling, the displayed or transmitted weight can lag behind the changing load. If a dosing controller closes a valve based on that delayed signal, material continues entering before cutoff. Material already travelling toward the vessel adds further overshoot.
This creates a practical distinction between static weighing and active batching. A stationary load can often be measured after a suitable settling period. A dosing system must make decisions while mass is changing, so a filter that works well for a static check may impair ingredient control.
Frequency-selective filters can reduce a persistent disturbance when its frequency is sufficiently stable and distinguishable from useful measurement changes. Their benefit becomes less predictable when machine speed varies, several sources operate together, or the structure resonates across different operating states.
Sampling also matters. If unwanted vibration components reach the measurement chain without suitable anti-aliasing protection, they can appear in sampled data as misleading lower-frequency variations. A high display update rate alone does not establish that the acquisition and filtering stages handle vibration correctly.
Ask how the instrument determines “stable,” whether the control output uses the same signal as the display, and how much response delay the selected settings introduce. A stability flag usually means that a defined signal criterion has been met. It does not independently establish that the indicated mass is correct.
Match the remedy to the disturbance
The most effective correction often begins at the source: repair rotating equipment, correct imbalance, eliminate loose supports, or separate a vibrating machine from the weighing structure. These actions reduce the disturbance before signal processing becomes necessary.
Structural changes require more care than simply making everything heavier or adding softer mounts. Increasing stiffness can reduce frame deflection and move a natural frequency, but it can also change how vibration is transmitted. Adding mass changes the dynamic response and may increase the inertial forces associated with a given acceleration.
Vibration isolators are appropriate only when their dynamic behavior suits the installation. Near an isolation system’s natural frequency, motion can be amplified. Effective isolation occurs within a suitable frequency range, and its performance depends on the supported mass, stiffness, and damping.
Soft pads can also permit rocking, extend settling time, or allow connected pipes to restrain the vessel. For some installations, a rigid independent support performs better than a soft mounting arrangement. Select isolation using the excitation frequencies and load range, then check that all connections accommodate the resulting movement.
Accelerometer measurements can help identify sources and resonances, especially when recorded alongside weighing signals. However, floor acceleration alone cannot predict weighing error. The relationship depends on the transmission path, structure, load-cell mounting, and signal processing. Measurements at the foundation and weighing assembly provide a more useful comparison.
Validate performance within the production cycle
A calibration check with nearby equipment stopped establishes a useful baseline. It does not demonstrate that the system can weigh accurately during a normal cycle. Site testing should connect the measurement result to an operating state, an allowed error, and a defined decision time.
- Define the process requirement. State the acceptable error for the actual quantity being controlled, including small additions into a large vessel. Specify when the controller must obtain the result.
- Establish a quiet baseline. Check zero, known loads, repeatability, and return to zero under controlled conditions. This helps separate vibration effects from existing calibration or mechanical problems.
- Introduce disturbance sources separately. Run relevant conveyors, pumps, mixers, and nearby machinery individually where practical, then in realistic combinations.
- Test representative load states. Include conditions that change supported mass, material movement, or structural response. Examine startup, shutdown, filling, discharge, and speed changes.
- Record timing and error together. Capture indication variation, available unfiltered or minimally filtered signals, stability status, controller decisions, and final settled results.
- Repeat complete cycles. Assess both average error and variation between cycles. A satisfactory average can conceal inconsistent batches.
Keep settings consistent during comparisons and document any changes to filtering, stability thresholds, or control logic. Otherwise, an apparent improvement may reflect a longer measurement time rather than better performance within the required cycle.
For batching, independently check the delivered quantity using a suitable reference method with adequate measurement capability. Comparing a controller’s cutoff reading with its own final display helps diagnose timing effects, but it does not establish accuracy against an independent reference.
For moving-product weighing, include representative products, speeds, spacing, and conveyor transitions. Empty-belt behavior and stationary test loads cannot capture all forces created as products enter and leave the weighing section.
What specifications and standards actually establish
“High precision” does not define a complete performance requirement. Display resolution describes the smallest indicated increment; it does not establish accuracy under vibration. Load-cell specifications likewise describe a component under stated conditions, while installed performance also depends on mounting, structure, connections, electronics, and operating sequence.
Distinguish static measurement error, repeatability, settling time, and dynamic process error in the acceptance specification. Each answers a different question. A system can repeat consistently with a bias, achieve acceptable accuracy after a long wait, or pass a stationary check while failing at production speed.
The applicable metrological framework depends on the instrument’s function and use. Nonautomatic weighing, automatic checkweighing, and automatic filling involve different operating conditions and performance assessments. Where measurements support regulated transactions, instrument approval and verification requirements must be addressed alongside installation performance.
A component certificate does not establish that the assembled installation meets its required performance. Similarly, passing defined instrument tests does not quantify every disturbance present at a particular site. The purchase specification should identify the operating conditions and require demonstrated performance under them.
Before comparing suppliers, establish the smallest critical quantity, permissible error, available measurement time, and machinery that will operate during weighing. Ask for evidence covering that combination. Those conditions determine whether better mounting, source control, isolation, filtering, or a different weighing arrangement is needed—and whether the proposed system can produce a reliable result when production is running.