
Food batching failures are rarely caused by a single inaccurate scale. More often, the problem sits at the intersection of hygienic design, material behavior, operator handling, recipe logic, and incomplete production records. A system can meet a stated weighing tolerance in a clean test environment yet still create inconsistent batches when powders bridge in a hopper, washdown reaches an unsuitable junction box, or manual additions are recorded outside the production database.
For food manufacturers, selecting an industrial weighing system is therefore not simply a capacity-and-resolution exercise. The system must measure the right amount, keep the product zone cleanable, control how ingredients enter the batch, and preserve a defensible record of what was actually used. These requirements become more demanding where allergens, high-care production, frequent recipe changes, small-dose ingredients, or regulated label claims are involved.
Start with the batch decision, not the scale specification
The most useful starting point is to map the actual batching decision. Is the equipment verifying incoming ingredients, dosing several materials into a mixer, filling a premix vessel, checking package weight, or reconciling material consumption against a production order? Each task imposes different technical requirements.
A hopper scale used for bulk flour addition may need high throughput, stable readings under vibration, and a design that prevents product accumulation around load cells. A micro-ingredient station for salt, seasoning, enzymes, colors, or processing aids may prioritize low-end resolution, controlled dispensing, operator confirmation, and closed handling. A loss-in-weight feeder is selected less for a final static mass than for its ability to maintain a controlled mass flow rate over time. Treating these applications as variations of the same weighing problem leads to poor equipment choices.
Technical evaluation should define the following before comparing suppliers:
- Ingredient types, including bulk solids, fine powders, liquids, pastes, and particulate inclusions.
- Minimum and maximum addition quantities for each ingredient.
- Required batch size, throughput, and the permitted time for each weighing operation.
- Whether each ingredient is automatically dosed, manually added, or verified after addition.
- Cleaning method, cleaning frequency, water exposure, and whether chemical foams or high-pressure washdown are used.
- Required electronic records, exception handling, and integration points with recipe or enterprise systems.
This definition exposes a common mismatch: selecting a high-capacity platform because the total batch is large, while overlooking that the system must also verify a very small ingredient. A load cell may have adequate capacity but insufficient usable resolution at the low end of the operating range. Conversely, a highly sensitive small scale may be easily overloaded, slow to settle, or too unstable for a vibrating production floor. In many formulations, separate weighing ranges or dedicated micro-dosing equipment are more reliable than forcing one instrument to cover every task.
Accuracy is a process characteristic, not a display value
Readability, repeatability, linearity, and overall batch accuracy are related but not interchangeable. A display increment of 1 gram does not prove that the process can repeatedly dose an ingredient within 1 gram under live operating conditions. Air currents, mixer vibration, product impact, feeder pulsing, mechanical friction, temperature effects, and unstable material flow can all affect the final result.
The relevant question is whether the completed addition stays within the recipe’s allowable tolerance. That requires examination of the full dosing sequence: the scale’s response, feeder behavior, coarse and fine feed transitions, material flight time, gate closure response, and the method used to confirm the final weight.
Free-flowing granules can often be controlled with a straightforward coarse/fine feed arrangement. Fine powders may continue falling after a screw feeder stops. Sticky or cohesive ingredients may discharge inconsistently because of bridging, rat-holing, or residue on contact surfaces. Liquids can dribble from valves, especially where viscosity changes with temperature. These effects are not corrected by specifying a more precise load cell alone.
For each critical ingredient, the evaluation should require a practical dosing test across the intended operating range. The test should include repeated small, nominal, and large additions; not just one target setpoint. It should also assess the impact of a full versus nearly empty source hopper, because feeder behavior can change as head pressure and material level change. Where formulation limits are tight, the control system should support target adjustment, tolerance bands, overshoot alarms, and an explicit rule for what happens when a dose falls outside tolerance.
Batch consistency also depends on the scale’s mechanical installation. Load cells need a defined load path. Pipework, flexible connections, access platforms, cable trays, or guarding must not introduce side loads or bind the vessel. A rigid pipe connected directly to a weighed tank can create a hidden bypass path that distorts measurements. Flexible connectors help only when they are correctly sized, aligned, and maintained. In hygienic batching, mechanical details often determine whether calibration remains meaningful after installation.
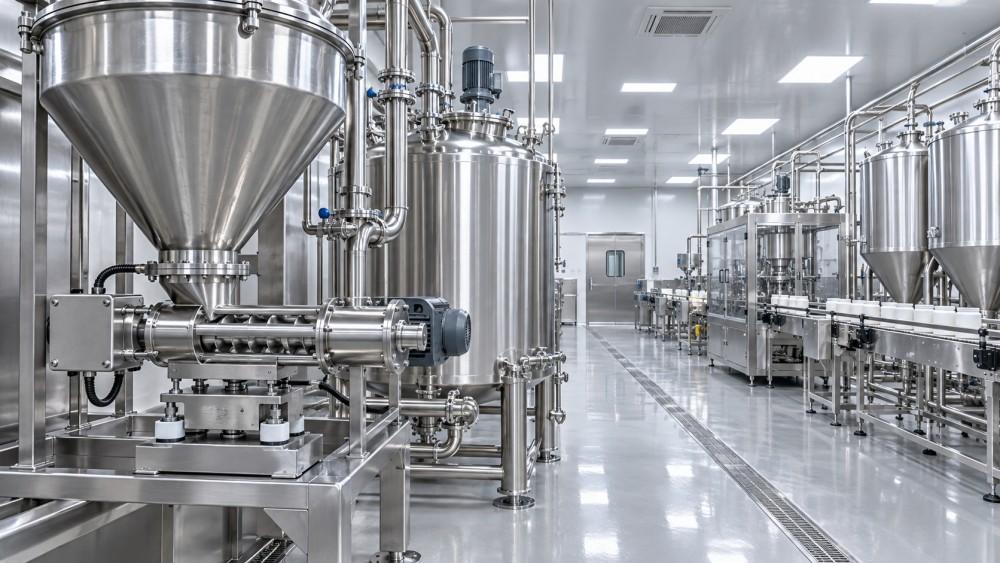
Hygienic construction must be assessed as a cleanability system
Food-grade stainless steel alone does not make a weighing system hygienic. The more important question is whether product-contact and adjacent surfaces can be effectively cleaned, inspected, and dried within the plant’s sanitation regime.
Design review should look for horizontal ledges, unsealed crevices, exposed threads in product areas, overlapping sheets, inaccessible framework, and hollow sections that can retain moisture or debris. Product zones should drain where wet cleaning is used, while dry-product systems need geometry that minimizes powder retention and permits practical dry cleaning. A design optimized for washdown can be unsuitable for hygroscopic powder if water ingress creates caking or microbiological risk in difficult-to-dry areas.
Material selection also needs to reflect the real cleaning chemistry. Commonly used stainless grades may perform differently when exposed to chlorides, acidic cleaners, alkaline agents, or repeated thermal cycles. Surface finish, weld quality, gasket material, and the compatibility of seals with cleaning agents matter as much as the main hopper material. If a supplier states that a system is “washdown rated,” the evaluation should clarify which parts are covered: load cells, connectors, junction boxes, cable glands, operator terminals, drives, and local control panels may have different protection ratings and limitations.
Where hygienic design standards are relevant to the facility or customer specification, references to recognized schemes such as EHEDG guidance or 3-A Sanitary Standards can provide a structured basis for review. They should not be treated as interchangeable global legal requirements. The correct criterion is the applicable food safety plan, customer requirements, local regulations, and the particular product risk.
Load cell placement deserves special attention. Cells mounted beneath an open vessel are easier to inspect, but may be exposed to water, dust, impact, or chemical spray. Protected mounting arrangements can improve durability but may make sanitation and inspection harder. The best arrangement balances access, cleanability, load integrity, and maintenance safety rather than maximizing enclosure alone.
Traceability depends on transaction design
Traceability is often described as a software feature, but it is fundamentally a transaction-control problem. The record must show not merely the intended recipe, but the production event that occurred: which order was made, which recipe version was active, which lots were selected, what quantities were weighed, whether tolerances were met, and how deviations were handled.
A robust electronic batch record commonly links:
- Production order or batch identifier;
- Recipe revision and approved target values;
- Ingredient identity and supplier or internal lot number;
- Actual weighed quantity, timestamp, and weighing point;
- Operator identification where manual action is involved;
- Alarms, overrides, substitutions, rework additions, and corrective actions;
- Calibration or verification status of the weighing equipment used.
Capturing these data points is not enough if they can be changed without accountability. System permissions, audit trails, electronic approvals, and controlled recipe editing are particularly important where batches support allergen segregation, nutritional declarations, infant nutrition, export documentation, or customer-specific formulation controls.
Integration should be evaluated at the level of data ownership. A standalone scale controller may store local records, but the plant may need master recipes controlled by manufacturing execution software, an ERP platform, or a quality management system. Determine which system creates the batch ID, where ingredient lots are validated, and where the final batch record is retained. Ambiguity in these handoffs leads to duplicate entries and reconciliation work.
The communication method matters as well. Common industrial interfaces may be adequate for weight transmission, but recipe management, lot validation, alarms, and audit data require a clearly defined data model. A statement that the equipment “connects to ERP” is not a specification. The technical review should identify fields, message direction, update timing, error handling, offline operation, synchronization after connection loss, and responsibility for interface maintenance.
Manual additions are often the weak point
Automated bulk ingredients tend to receive the most engineering attention, while manual additions create the largest traceability and formulation-control exposure. A paper tick sheet beside a bench scale may be sufficient for a low-risk operation, but it is weak evidence when the process requires lot control, allergen confirmation, or strict sequencing.
A manual weighing station can be designed to reduce these failures. Barcode or RFID scanning can confirm the ingredient and lot before weighing. The workstation can display the required target and tolerance, prevent the operator from proceeding with the wrong material, and record actual net weight after tare verification. For ingredients delivered in bags or containers, the system should distinguish gross weight, tare weight, and net addition. This is especially important where packaging tare varies between lots or where partial containers are returned to storage.
The physical workflow should support the electronic logic. If several similar-looking ingredients can be staged at the same station, the risk of a correct barcode scan followed by the wrong physical scoop remains. Segregated staging, controlled container identification, and clear disposition of opened packs are process requirements, not optional software enhancements.
Calibration control should match the consequence of error
Calibration is often requested as a certificate at commissioning, then treated as a maintenance formality. In a food batching system, calibration control should demonstrate that the installed system remains fit for its actual use range and tolerance requirements.
Verification points should include the low range where critical minor ingredients are weighed, not only a convenient mid- or high-range test load. A scale used from 2 kg to 1,000 kg cannot be meaningfully assessed by a single check near its maximum capacity. The test method should also account for the installed mechanics: vessel restraints, flexible connections, feeder supports, and environmental vibration can influence in-service performance even when a scale indicator performs correctly on a bench.
Calibration intervals should be set through a documented risk-based approach. Factors include product criticality, use frequency, cleaning severity, vibration, likelihood of mechanical damage, historical stability, and the ability to detect a fault before product release. Between formal calibrations, routine verification with suitable reference weights or controlled checks can detect drift, but only if the plant defines acceptance limits and clear escalation actions.
Reference weights require their own control. Their traceability, handling, protection from damage, and storage conditions affect the credibility of the verification program. A test weight left in a wet processing area or repeatedly dropped onto concrete should not be assumed reliable.
Evaluate the system during sanitation, maintenance, and fault recovery
The best time to identify weak design choices is before purchase, when the supplier can demonstrate how the equipment is opened, cleaned, inspected, reassembled, and returned to service. Request a review of routine access points: hopper interiors, feeder screws, valves, seals, dust extraction interfaces, load cells, cable routing, and drain points. The question is not whether components can theoretically be removed, but whether this can be done safely and consistently within the site’s available shutdown window.
Cleaning can also affect measurement. Disassembly may alter the position of flexible connections. Water retained on a vessel or product residue left after cleaning changes tare conditions. Reassembly errors can create mechanical interference. A suitable control strategy includes post-cleaning checks where needed, controlled tare procedures, and guidance on when a scale must be reverified before production resumes.
Fault recovery deserves equal attention. If a network connection fails, can the line continue operating? If it does, how are batch records protected and reconciled? If a load cell signal becomes implausible, does the controller stop dosing, allow a controlled hold, or permit manual fallback? A manual fallback procedure without independent verification can protect throughput while undermining traceability. The acceptable response depends on process risk and must be defined before commissioning.
Selection should result in a defensible acceptance basis
A technically sound purchase specification converts operational needs into testable acceptance criteria. Rather than requiring a generic “accurate, hygienic, traceable” system, define the ingredients, target ranges, dosing tolerances, throughput, cleaning exposure, material-contact requirements, data fields, access permissions, interface responsibilities, and verification methods that the system must meet.
Factory acceptance testing is useful for controller logic, recipe handling, alarms, and data records, but it cannot fully prove performance with the plant’s actual ingredients and installation conditions. Site acceptance should confirm dosing behavior, mechanical freedom, sanitation access, network operation, electronic records, and calibration performance after installation. Any performance claim should be tied to the specified material and operating conditions; a system proven with free-flowing salt is not automatically proven for a cohesive seasoning blend.
The right food industrial weighing system is the one whose measurement range, mechanical design, sanitation regime, and record architecture all support the same process. When those elements are evaluated together, batching equipment becomes more than a device for displaying weight: it becomes a controlled point for recipe execution, food safety assurance, and reliable production evidence.