
Pharmaceutical batch accuracy depends on controlling the small errors that accumulate before a blend reaches compression, filling, or packaging. A minor weighing error in a potent active ingredient, an unrecorded container tare, residual powder in a transfer line, or a material substitution that looks similar on a label can shift dose uniformity and create a difficult investigation later. In Indian facilities handling multiple products, strengths, and pack formats, the strongest controls connect material identity, measured mass, equipment status, and batch records at the point where each action occurs.
Reliable pharmaceutical batching accuracy in India begins with a practical premise: a scale display alone does not prove that the correct material, correct quantity, and correct destination have been controlled. Those conditions must be verified together. The process should also distinguish a true weighing discrepancy from loss during handling, moisture-related mass change, dispensing residue, or a record-entry error. Treating all of these as “weighing deviations” obscures the corrective action.
Control the weighing event, not only the final total
Batch records often contain a target quantity and an acceptable tolerance, but the control point is the individual dispense. Each dispense should have a defined material code, lot identity, unit of measure, target mass, container identification, scale identification, and time-linked confirmation. When these elements are captured separately, a discrepancy can be localized. Without that separation, a correct final total may conceal a wrong lot, an omitted component later added from memory, or an ingredient charged to the wrong vessel.
For low-dose ingredients, the selected balance must match the intended sample size. A large platform scale can be suitable for excipients in bags or drums while being unsuitable for a small quantity of colorant, preservative, or potent active. Resolution is only one part of the decision. Repeatability at the normal dispensing load, minimum usable load, environmental stability, and the effect of air currents or vibration all affect whether the reading is dependable.
A useful control sequence is to establish the empty container tare, place the material in the container, verify the gross and net values, and lock the transaction before the material leaves the dispensing station. Re-taring after material has been added should require a documented reason because it can conceal an earlier handling mistake. Where manual transcription remains necessary, the displayed value should be independently verified before it is entered rather than reconstructed from a label or memory after the container has moved.
Mass is not always the same as delivered quantity
A scale may show an accurate net mass while the actual amount transferred to the blender is lower. Fine cohesive powders can cling to scoops, liners, funnel walls, and discharge valves. Hygroscopic materials can gain mass during an extended open handling period. A dense granule can clear a container cleanly while a low-bulk-density powder leaves a visible but hard-to-quantify residue. These conditions require different controls.
- For materials with predictable adhesion, define whether the container is intended to be fully discharged, rinsed into the process where permitted, or weighed back after transfer.
- When exposure to ambient humidity affects material behavior, limit open-container time and record the actual dispensing interval when an excursion is investigated.
- Use dedicated or suitably cleaned transfer tools for ingredients where carryover is a realistic risk; a visually clean scoop is not evidence that residues are absent at a relevant level.
- For pre-weighed kits, preserve the connection between each sealed inner container and the batch until charging is complete. Separating labels from containers creates avoidable reconciliation problems.
Reconciliation should compare more than theoretical issue quantity against returned quantity. It should account for retained samples, approved processing losses, material remaining in dispensing containers, and any partial container used across batches. A reconciliation result that appears acceptable only because multiple unmeasured residues were assumed should be investigated before the next batch begins.
Make material identity difficult to bypass
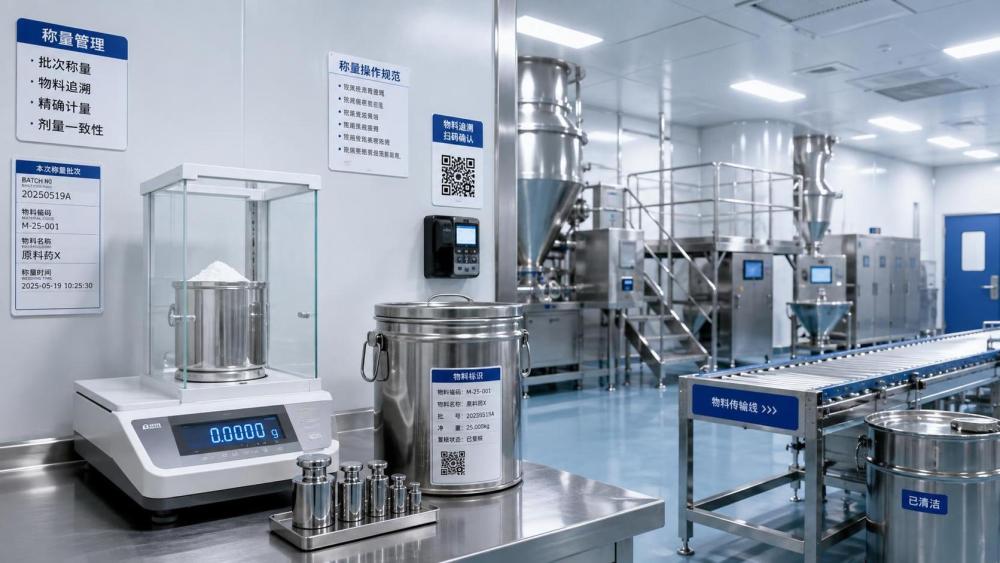
Look-alike containers, similar product names, different grades of the same excipient, and multiple active strengths create a risk that cannot be solved by weighing accuracy alone. Two white powders may reach the same target mass and still produce a nonconforming batch. Identity controls need to function before dispensing, during staging, and at the charging point.
Segregated staging locations reduce mix-ups when several batch orders are active. Each staged material should remain physically associated with a clear batch-specific status label. Labels need enough information to distinguish the internal material identity, source lot, released status, quantity, and intended batch; relying on a handwritten short name is fragile when names are similar. Barcode or other machine-readable verification can strengthen this control, provided the scan confirms the material and transaction rather than merely printing a label.
Charging is a separate verification point. A correctly weighed container can still be placed beside the wrong blender, emptied in the wrong sequence, or held long enough to lose its status. At the vessel, confirmation should connect the container identity to the batch and formula step. For multi-component additions, the record should make omissions visible. A blank signature field after a long list of components is weak evidence that every item was charged.
Set tolerances around the formulation and the process capability
A single percentage tolerance for every component is convenient, but it can be technically misleading. The same percentage error has a very different dose impact for a low-level active ingredient than for a bulk filler. Conversely, an extremely narrow tolerance on a high-volume excipient can create repeated rework without improving the critical quality attribute. Tolerances should reflect the formulation role, intended concentration, measurement uncertainty, and the smallest meaningful adjustment that can be made during dispensing.
An out-of-tolerance result should not automatically lead to topping up or removing material. First establish whether the error is in the measurement, the tare, the target selection, or the physical dispense. Adding material to correct a suspected underweight can create a second error if the original reading was affected by an unstable scale or incorrect container setup. The defined response should state who assesses the discrepancy, what evidence must be retained, and when the batch step must stop.
Keep scales accurate under actual operating conditions
Calibration status is necessary but does not demonstrate that a balance is performing correctly at the time of use. Daily or shift-start verification using suitable reference weights can identify drift, damage, leveling problems, contamination, or a display fault before material is dispensed. The reference load should be meaningful for the balance and the normal operating range. A large test weight offers limited assurance for a balance used to weigh very small additions.
Scale placement deserves the same attention as calibration. Drafts from doors, air-conditioning outlets, or extraction hoods can disturb sensitive weighing. Vibration from nearby granulators, forklifts, or building movement can cause unstable readings. A bench that flexes under a drum or an uneven floor beneath a platform scale can create repeatable error that appears to be operator inconsistency. Equipment verification records should note abnormal repeatability or stabilization time, not only pass or fail status.
Cleaning methods can also affect performance. Powder buildup beneath a weighing pan, damaged load-cell cabling, aggressive washdown near unsuitable equipment, and solvent ingress can change response without producing an obvious alarm. After maintenance, relocation, or a significant cleaning event, a documented return-to-service assessment should confirm the scale is level, stable, properly identified, and linked to the intended electronic or paper record.
Design the flow to prevent contamination and confusion
Accuracy is undermined when the dispensing room becomes a temporary warehouse of open containers, labels, tools, and documents. Limit the number of active materials at a station, remove finished components before the next material is opened, and maintain clear physical separation between pending, in-process, and completed dispenses. The sequence is especially important for sensitizing materials, potent compounds, and products with low permitted carryover.
Cleaning verification should address the equipment surfaces that contact material, including scoops, funnels, transfer chutes, liners where reused, and container closures. A good visual inspection remains useful for gross residue, but it should not replace a defined cleaning and verification approach when residues could affect the next product. The batch process also needs a way to prevent cleaning tools, waste containers, or prior-product labels from returning to the dispensing area unnoticed.
Environmental controls should be tied to material behavior rather than treated as generic housekeeping. Fine powders may disperse when air velocity is too high; static charge can make powders adhere to polymer liners and utensils; excessive humidity can promote clumping and alter flow into a container. These observations matter because a poor flow pattern can produce a misleading assumption that a container was fully emptied or that a scoop delivered a consistent quantity.
Use records to reveal process weakness early
Electronic batch records, connected scales, and barcode checks are valuable when their workflow matches the physical process. A system that permits a transaction to be completed before the material is actually dispensed creates a false sense of traceability. Likewise, a manual backup form should preserve the same critical fields and reconciliation logic when electronic equipment is unavailable. Parallel records with different values are a deviation signal, not an administrative inconvenience.
Trend review should separate recurring causes: repeated minor underweights on one balance, frequent corrections on a particular material, unusually high container residue, or identity confirmations that occur late in the process. Each pattern points to a different weakness. Recurrent issues with one powder may indicate flow, static, or packaging characteristics. A cluster around one shift or room may indicate training, layout, lighting, or equipment condition. A pattern of exact target weights on manually dispensed materials can also warrant review if normal process behavior would reasonably show small variation.
Batch accuracy becomes more robust when the record tells the same story as the material movement: the released lot was staged, the correct quantity was weighed on suitable equipment, the container was identified through transfer, the intended material was charged, and any discrepancy was evaluated before processing continued. That chain of evidence reduces dose variability while making deviations easier to understand and correct.