
A formulation can look stable on paper and still drift on the factory floor. The reason is often hidden in the smallest ingredients: pigments, catalysts, stabilizers, flavors, active compounds, conductive carbon, curing agents, or other additives that make up only a small fraction of the batch but have an outsized effect on the finished product.
For technical evaluators, specifying precision batching systems for additives is therefore not a matter of selecting the feeder with the most impressive nominal accuracy figure. The real question is whether the complete system can repeatedly deliver the required amount of a real, often difficult material, at the actual production rate, while preserving records that quality and compliance teams can trust.
Tight dosing tolerances bring together mechanical design, material science, weighing technology, automation logic, and operating discipline. A system may perform well during a supplier demonstration with a free-flowing reference powder, then struggle when exposed to hygroscopic ingredients, low bulk density fibers, sticky concentrates, or frequent recipe changes. A sound specification anticipates those conditions before equipment is purchased.
Start with the process tolerance—not the feeder brochure
The first specification decision is to define what “tight” means in the context of the process. This sounds obvious, but many projects begin with an isolated request such as “±0.5% dosing accuracy” without clarifying the basis of that percentage. Is it measured against the individual additive target, the total batch mass, or the finished product specification? Those are very different requirements.
For a 5 kg additive target, a small deviation may be manageable. For a 20 g catalyst addition in a large vessel, the same percentage-based statement can conceal a much more demanding absolute error. The smallest required dose frequently determines the architecture of the batching system, not the largest one.
Technical teams should document the following before evaluating equipment:
- Target dose range for every additive, including the smallest routine and occasional dose.
- Permissible deviation in both absolute units and percentage terms.
- Batch frequency, required cycle time, and allowable time for correction or verification.
- Whether additives are dosed individually, premixed, or added in sequence.
- Consequences of underdose, overdose, missed dose, and wrong-material addition.
- Requirements for lot traceability, electronic batch records, and audit review.
This process definition prevents a common mismatch: purchasing a high-resolution scale while overlooking feeder controllability, refill disturbance, or the practical repeatability needed at the discharge point.
Accuracy, repeatability, and resolution are not interchangeable
Equipment discussions often use these terms loosely. They should be separated in the specification because they describe different risks.
Resolution is the smallest increment the weighing system can display or detect. A fine display division does not automatically mean the system can dose accurately. Electrical noise, vibration, mechanical friction, and unstable material flow can make apparently fine resolution meaningless in operation.
Repeatability describes how consistently the system reaches the same result over repeated cycles. For production, this is usually more revealing than a single successful test run. If the feeder produces a changing flow pattern from one cycle to the next, control software may compensate only partially.
Accuracy compares the measured or delivered amount with a known reference. It depends on calibration, load-cell behavior, mechanical layout, control strategy, and how the final dose is verified. It should be stated with operating conditions, dose size, material, test method, and measurement uncertainty—not as a standalone marketing number.
A robust request for quotation asks suppliers to state performance at representative minimum, nominal, and maximum doses. It should also distinguish between static scale accuracy and dynamic batch dosing performance. The latter is what matters when material is flowing, valves are closing, screws are decelerating, and the scale is reacting to the last few grams.
Material behavior often decides the feeder choice
The additive itself is not a minor detail attached to the equipment specification. It is the starting point. Powders that bridge, compact, segregate, absorb moisture, electrostatically cling to surfaces, or release in pulses will challenge even a well-designed gravimetric system.
Characterize each material as it will arrive and be used, rather than relying only on a safety data sheet. Bulk density range, particle size distribution, moisture sensitivity, flowability, angle of repose, tendency to cake, and dust behavior all influence feeder selection. So do packaging format, storage duration, ambient humidity, and whether the material is recycled, reclaimed, or freshly supplied.
For free-flowing granular additives, a loss-in-weight feeder or controlled screw feeder may provide stable performance with relatively straightforward agitation. Fine cohesive powders may require hopper conditioning, bridge breakers, agitators, flexible hopper walls, or twin-screw configurations designed to avoid compaction. Fibrous materials and low-density powders can demand a very different feeding mechanism from dense mineral additives, even when the target dose is similar.
Liquid additives create another set of concerns: viscosity changes with temperature, pump pulsation, hose elasticity, valve dribble, entrained air, and residual material left in lines. A system specified only around pump capacity may overlook the accuracy loss caused by these practical effects. In some applications, weighing the receiving vessel or using a mass-based verification step is more dependable than trusting volumetric delivery alone.
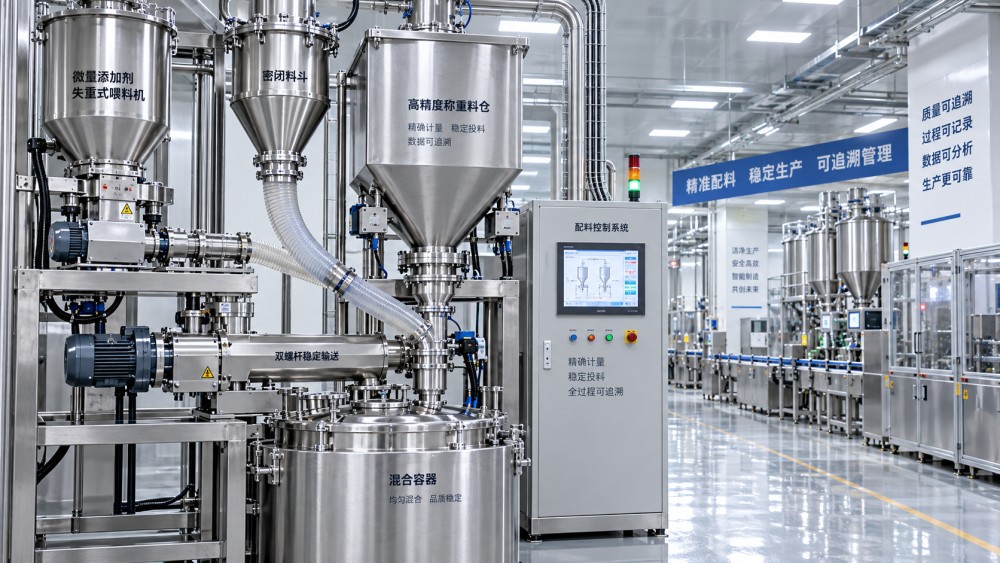
Choose the batching architecture around the critical addition
There is no single “best” design for tight-tolerance dosing. The appropriate architecture depends on whether the process is batch-based or continuous, whether additives share a destination, and whether production priorities favor speed, containment, flexibility, or maximum verification.
Gain-in-weight batching measures material added to a receiving vessel or weigh hopper. It is often suitable where a defined batch is built sequentially and where each component must be recorded before the next step begins. The method can offer clear batch accountability, but accuracy depends on vessel isolation, residual material management, and avoiding unintended forces from connected pipes, cables, or agitators.
Loss-in-weight feeding measures the reduction in mass from the feeder and hopper assembly. It is particularly useful for controlled continuous addition and can also support highly repeatable small-dose delivery. However, refill periods need careful management. During refill, the system may temporarily lose direct gravimetric control or shift operating mode, so the impact on the process must be understood rather than assumed away.
Volumetric feeders may have a place when tolerances are wider, materials are highly consistent, or a gravimetric check is used downstream. They should not be dismissed automatically, but they should not be treated as equivalent to gravimetric dosing when material density and flow behavior vary.
For particularly sensitive formulations, a two-stage dosing strategy deserves consideration. A feeder delivers most of the target at a faster rate, then transitions to a dribble or trim phase as the target approaches. The transition point, cutoff logic, and compensation for material “in flight” are central to final performance. Faster is not always better: an aggressive coarse-feed stage can create an overshoot that no trim phase can recover.
Specify the weighing system as an installed system
Load-cell capacity and scale resolution are only part of the decision. A load cell should be selected with enough useful signal at the smallest dose while retaining capacity for the vessel, feeder, material inventory, and realistic upset conditions. Oversizing the scale to accommodate unlikely loads can reduce sensitivity where it is needed most.
Mechanical integration deserves equal scrutiny. Side loads, rigid pipework, hose tension, product buildup, floor vibration, air currents, and maintenance access can all affect weighing behavior. A scale may be accurate on a test stand but unstable after installation beside a mixer, conveyor, or pneumatic conveying line.
Ask how the supplier handles:
- Isolation from structural vibration and feeder motor disturbances.
- Flexible connections between weighed and fixed equipment.
- Dust extraction without creating unwanted forces on the weighed vessel.
- Grounding and electrostatic control for fine powders.
- Level indication that does not compromise the weighing signal.
- Access for cleaning, inspection, calibration weights, and feeder removal.
Where the dose is very small relative to the vessel tare weight, consider whether a dedicated micro-ingredient scale or feeder is justified. Combining all additive ranges onto one large scale can simplify the layout but may make the smallest additions harder to control and verify.
Control logic is where mechanical capability becomes production consistency
Precision batching systems for additives need more than a target setpoint. Their controls should govern recipe permissions, dosing sequence, tolerances, alarms, correction rules, operator prompts, and record generation. The best arrangement reflects the actual risk profile of the formulation.
A useful control philosophy distinguishes between warning limits and reject limits. A minor deviation may trigger review or supervised correction; a more serious deviation may lock the batch, prevent downstream transfer, or require a documented disposition. The appropriate response should be agreed with production and quality teams in advance. Leaving these decisions to informal operator judgment can weaken the value of an otherwise capable dosing system.
Recipe management also deserves attention. Evaluators should determine who can create, edit, approve, and release a formula; whether changes are version-controlled; and whether an operator can substitute a material without authorization. Barcode or RFID-based material identification can reduce wrong-additive risk, especially where similar bags, drums, or supplier labels are present.
For regulated, export-sensitive, or high-value manufacturing, the system may need to retain time-stamped records of lot identity, target quantity, actual quantity, deviations, operator actions, calibration status, and batch disposition. Integration with MES, ERP, laboratory systems, or plant historians should be defined early. Data transfer is not merely an IT feature when it determines whether a batch can be investigated months later.
Calibration is a lifecycle requirement, not a commissioning event
Every weighing system drifts over time due to wear, environmental change, cleaning practices, accidental impacts, and modifications to the process. Tight-tolerance applications need a calibration plan that is realistic for the plant, not just technically possible for the supplier.
Specify how zero checks, span checks, and full calibration will be performed; what certified test weights or reference methods are required; and how results will be recorded. For feeders, calibration should include delivery performance, not only the scale signal. A correctly calibrated load cell cannot compensate for a screw feeder that has begun to pulse because of material buildup or worn components.
It is also worth defining triggers for unscheduled verification: a feeder changeover, a significant maintenance event, an abnormal batch trend, a control fault, or a formulation complaint. This protects the process from the quiet degradation that can occur between routine calibration intervals.
Demand an acceptance test that resembles production
Factory acceptance testing is valuable, but it should not be the final proof of performance. A meaningful site acceptance test uses representative materials, actual packaging and refill methods, expected environmental conditions, and production-relevant recipes. If the plant cannot supply the exact material in advance, the limitation should be visible in the project risk register rather than forgotten.
The acceptance protocol should define the number of consecutive dosing cycles, target quantities, allowable deviations, refill conditions, changeover conditions, and how results will be measured. It should test ordinary operation as well as plausible disruptions: low hopper level, restart after a pause, material lot change, and transition between coarse and fine feed.
Review trends, not just pass/fail results. A system that technically meets tolerance but shows gradual drift across consecutive batches may be signaling a refill, compaction, or thermal issue that will become significant at scale.
Questions that reveal whether a proposal is genuinely comparable
When competing proposals appear similar, the most useful questions are often specific and uncomfortable. What material was used to establish the quoted dosing performance? At what dose and throughput? Does the stated tolerance include the effects of refill and discharge? How is residual material controlled? What happens if the target is exceeded? Which components require routine cleaning, and how long does a changeover take?
Also ask where the final quantity is measured. A feeder may accurately lose mass, yet material can remain in a discharge chute or adhere to a valve. In applications where the receiving vessel’s exact composition is critical, downstream verification may be more meaningful than feeder-side measurement alone.
Evaluators should resist proposals that solve every problem with software compensation. Predictive algorithms can improve performance, especially where flow behavior is stable, but they cannot eliminate poor hopper design, inappropriate feeder geometry, inconsistent material conditioning, or mechanical interference with the scale.
A specification that protects the formulation
The strongest additive batching specification does not simply request a machine. It describes a repeatable dosing outcome, the materials involved, the evidence required to prove that outcome, and the operating realities that could compromise it.
For manufacturers working with demanding recipes, precision is not just about reaching a number on a display. It is about ensuring that every batch can be trusted: the correct additive, in the correct amount, at the correct point in the process, with a record that stands up to quality review. By evaluating feeder behavior, weighing design, control logic, calibration discipline, and acceptance testing as one connected system, technical teams can select batching equipment that supports consistency long after commissioning is complete.