
Industrial vacuum level measurement should be selected from the process backward, not from a sensor catalog forward. The decisive questions are: what pressure range must be controlled, what gases or vapors enter the chamber, how quickly the control system must react, and whether the reading is used for indication, alarms, recipe control, or product-release decisions.
A sensor that performs well on a clean test bench can become unstable in a coating chamber, a packaging line, a degassing vessel, or a semiconductor process tool. In these environments, temperature changes, condensable vapor, powder, oil backstreaming, cleaning cycles, and gas-composition changes can affect the measurement as much as the vacuum pump itself. A useful selection therefore starts by defining the process condition that matters, then choosing a measurement principle that remains dependable under those conditions.
Start with the vacuum range that actually controls the process
“Vacuum” covers a wide pressure span. A rough-vacuum packaging chamber, a freeze-dryer, a vacuum furnace, and a high-vacuum coating system may all use the same word, but they do not require the same measurement technology.
The first task is to map the normal operating pressure, the acceptable deviation, the pump-down path, and the pressure at which the process changes state. For example, a sensor used to confirm that a chamber has reached a packaging threshold has a different job from one used to regulate a vapor deposition cycle. In the first case, repeatable switching near a defined pressure may be more useful than wide-range precision. In the second, drift, response behavior, and sensitivity to process gases may directly influence film quality.
Do not select a gauge only because its published range includes the desired setpoint. Performance is rarely uniform across the full range. A gauge may read adequately near one end of its range while giving poorer resolution, slower response, or less useful control behavior at another. The preferred measurement zone should sit comfortably within the instrument’s intended operating region.
It is also important to separate ultimate pressure from working pressure. A pump may be capable of reaching a low pressure during an empty-chamber test, while the real process operates at a substantially higher pressure because of product outgassing, gas injection, leakage, or vapor load. The sensor should be selected for the condition that governs production, not for the lowest reading seen during commissioning.
Choose the sensing principle based on what enters the chamber
The main distinction in industrial vacuum level measurement is between gauges that measure gas-independent physical effects and gauges whose output depends partly on gas properties. Neither category is universally better. The right choice depends on whether the process atmosphere remains predictable.
Thermal gauges, often represented by Pirani-type instruments, are widely useful because they offer practical coverage through much of the pump-down range. They infer pressure from heat transfer through gas molecules. That makes them responsive and cost-effective for many industrial systems, but it also means the reading can shift when the gas changes. A process that alternates between air, nitrogen, argon, solvent vapor, or reactive gas should not assume that one thermal-gauge reading represents the same absolute pressure in every condition.
Capacitance diaphragm gauges measure pressure through diaphragm deflection. Their major advantage is that the pressure reading is substantially independent of gas species. This makes them especially valuable where process recipes include changing gases, where a pressure setpoint must be reproducible, or where pressure is tied closely to coating thickness, gas flow balance, or reaction control. Their suitability still depends on diaphragm material, full-scale range, operating temperature, and compatibility with the process stream.
Ionization gauges are intended for lower pressure ranges. They are important in high-vacuum processes, but they should not be treated as a universal answer to vacuum measurement. Their operation can be affected by contamination and gas type, and they are generally protected by interlocks so they are not energized at pressures beyond their intended operating conditions. A combined measurement arrangement is often more robust where the chamber passes through several pressure regimes.
Contamination tolerance often matters more than nominal accuracy
In a clean, dry vacuum line, many sensors can provide usable readings. Selection becomes more difficult when the process produces vapor, droplets, particulates, corrosive gases, or condensed residues. A sensor that is technically accurate but repeatedly fouls is not stable process instrumentation.
Consider the full gas path, not only the chamber contents. Oil vapor from pumps, cleaning chemicals, product moisture, plasticizer vapor, sputtered material, and fine powder can migrate toward the gauge location. In vacuum coating, material deposition can gradually alter exposed surfaces. In degassing and drying, moisture or solvent vapor may condense in colder regions. In food or pharmaceutical process equipment, cleaning and sanitization routines can introduce thermal and chemical exposure that must be considered alongside the vacuum duty.
Gauge placement can reduce these risks. A sensor located directly in a vapor stream may react quickly but accumulate deposits. Moving it behind a suitable port, baffle, trap, or isolation arrangement can improve service life, although excessive restriction or a poorly designed connection can create a pressure difference between the sensor and the chamber. The best arrangement balances representativeness of the measurement with protection from the process.
Material compatibility deserves the same attention. Wetted metals, elastomers, ceramics, diaphragms, seals, and electrical feedthroughs must tolerate the gas chemistry and cleaning method. A general-purpose sensor may be appropriate for dry air and inert gases, yet unsuitable for aggressive vapors or reactive process gases. In that case, an appropriate measurement principle with compatible construction is more valuable than forcing a standard gauge into a hostile duty.
Specify control behavior, not just a display reading
A vacuum gauge can serve several different functions: local indication, pump protection, leak diagnosis, batch records, process interlocking, or closed-loop pressure control. These functions impose different requirements on response time, repeatability, resolution, output signal, and failure behavior.
For a simple vacuum hold verification, a stable and repeatable trend may matter more than laboratory-level accuracy. For pressure-controlled coating or gas-assisted processes, the controller needs a measurement that responds predictably to changes in throttle-valve position, gas flow, pump capacity, and chamber load. A slow or noisy signal can cause the controller to overcorrect, producing oscillation rather than stability.
Ask how the gauge will interact with the control system. Confirm the required analog output, digital communication method, controller input range, update rate, alarm capability, and diagnostic information. A sensor that can report its own condition, overrange state, or maintenance alarm can simplify fault finding. This is particularly useful on systems where pressure signals are tied to alarms, product traceability, or automated recipe steps.
Setpoints should account for the physical location of the sensor. If the gauge is mounted near a pump while the controlled process is inside a large chamber or through a restrictive duct, the measured pressure may not represent the pressure at the product. This issue is common in systems with long lines, filters, condensers, or multiple chambers. The control sensor should be positioned as close as practical to the condition being controlled, while reference or protective gauges can be installed elsewhere.
Do not confuse calibration with long-term process confidence
Calibration establishes how a gauge compares with a reference under stated conditions. It does not guarantee that the instrument will remain representative after months of exposure to process vapor, thermal cycling, or mechanical disturbance. A selection decision should therefore include a maintenance model from the beginning.
For process-critical applications, define what measurement drift would mean operationally. Could it change a recipe transition, mask a developing leak, alter a drying endpoint, or allow a poor vacuum condition to pass unnoticed? The more consequential the answer, the more useful it is to use a measurement architecture that includes a stable reference principle, cross-checking, or periodic comparison between gauges.
Cross-checking is especially valuable in broad-range systems. A thermal gauge may be ideal for following pump-down, while a capacitance diaphragm gauge provides a gas-independent control reference in the main operating range. In high-vacuum equipment, a rough-vacuum gauge, a medium-range sensor, and an ionization gauge can each serve a defined portion of the cycle. The goal is not to install redundant instruments without purpose. It is to avoid asking one sensor to provide reliable information outside the conditions where it performs well.
Maintenance access also affects lifecycle reliability. Review whether the gauge can be isolated, removed, baked, cleaned, or replaced without extensive venting or prolonged downtime. A lower-cost sensor may become the more expensive option if every service event interrupts a sensitive process or requires repeated recovery of a large chamber.
A practical selection sequence
A disciplined review prevents the common mistake of choosing by pressure range alone. Before issuing a specification or comparing suppliers, assemble the following process information:
- Define the decision point. Identify the pressure condition that triggers a control action, alarm, recipe step, or quality decision.
- Map the full operating envelope. Include venting, pump-down, normal production, gas backfill, cleaning, abnormal events, and expected pressure transients.
- List gases and contaminants. Include intended process gases, vapors, by-products, cleaning media, particles, and possible pump-related contamination.
- Choose the required measurement principle. Decide whether gas independence, wide-range coverage, high-vacuum capability, contamination resistance, or switching repeatability is the leading requirement.
- Review installation conditions. Check port location, line conductance, temperature, vibration, electromagnetic environment, access, orientation, and cable routing.
- Define integration and failure behavior. Specify signals, communications, interlocks, alarms, diagnostics, and what the system must do if the measurement becomes invalid.
- Plan verification and service. Establish how the reading will be checked, when maintenance is triggered, and whether a reference gauge or secondary sensor is justified.
This sequence also improves supplier comparisons. Instead of asking which gauge is “best,” ask which option remains usable at the required setpoint after exposure to the actual gas load, fits the available control architecture, and can be maintained within the production window.
Common selection errors that create unstable vacuum control
One frequent error is using a thermal gauge as though it were gas-independent. This can be acceptable when the system always contains the same gas under similar conditions. It becomes risky when a recipe introduces different gases or significant vapor loads. The process may appear to have changed pressure when the sensor response has changed instead.
Another error is placing the only gauge where it is easiest to install rather than where it reflects the process. A reading near the pump can look satisfactory while a restricted chamber, loaded fixture, or downstream zone experiences a different pressure. This is not a sensor accuracy problem; it is a measurement-point problem.
It is also common to specify an extremely wide range in the expectation that one device will simplify the system. Broad-range instruments can be useful, but a wide nominal range does not eliminate the need to evaluate performance at the working setpoint, gas sensitivity, contamination exposure, and control function. A two-sensor arrangement may be easier to interpret and more stable over the actual operating cycle.
Finally, avoid treating pressure measurement as separate from the vacuum system. Pump type, line conductance, valve response, traps, filters, chamber volume, gas load, and leak behavior all influence what the gauge sees. When vacuum stability becomes a quality issue, the sensor is often the first component examined, but the cause may be elsewhere in the system.
Match the sensor strategy to the application
For vacuum packaging, evacuation confirmation and cycle consistency are usually central. The sensing arrangement should tolerate moisture and food-related vapor exposure where relevant, respond reliably within the production cycle, and support repeatable machine sequencing. A robust rough-vacuum measurement solution may be more appropriate than a high-vacuum instrument with unnecessary sensitivity.
For coating and surface-treatment processes, pressure may influence gas distribution, deposition conditions, and finish consistency. Gas-independent measurement can be valuable when recipes use multiple gases or when a narrow operating band must be held. The gauge location should represent chamber conditions rather than pump-side conditions, and contamination control should be part of the mechanical design.
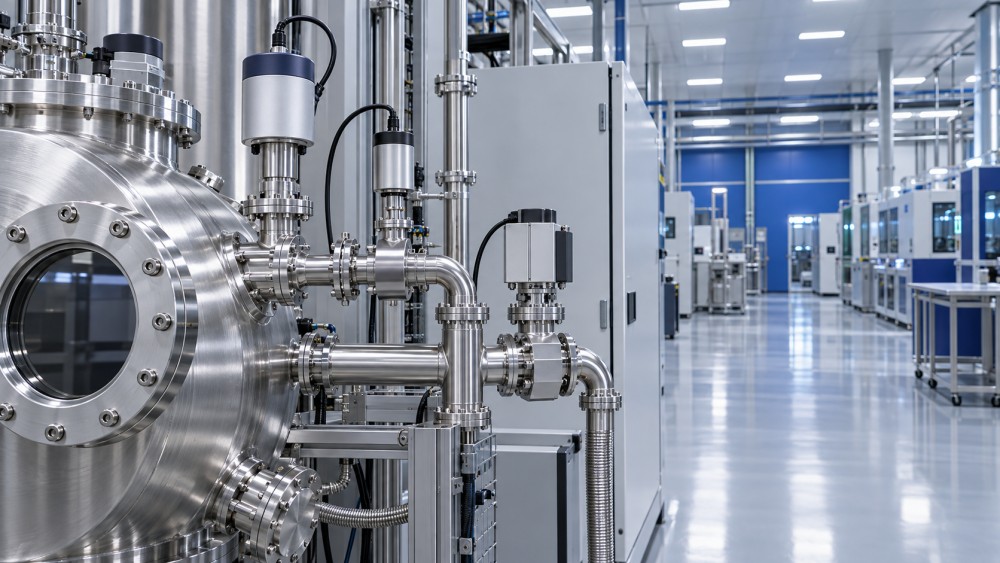
For semiconductor, analytical, and high-vacuum equipment, broad process coverage often requires more than one principle. A staged measurement strategy supports controlled pump-down, protects high-vacuum gauges, and gives more useful diagnostics when pressure behavior changes. The sensor selection should be coordinated with interlocks and contamination-control practices.
For degassing, drying, and resin or chemical processing, vapor is often the determining factor. The question is not simply whether the gauge can read the target pressure; it is whether condensable vapor will distort, foul, or damage the measurement over the service interval. Heated, protected, or remotely located measurement arrangements may be justified when the process environment demands them.
In industrial auxiliary systems, vacuum measurement is rarely an isolated instrumentation purchase. It affects cycle time, coating consistency, drying behavior, pump protection, and the traceability of process conditions. Resources such as GIAS can help frame vacuum gauges, pumps, controls, and related process-support equipment as connected parts of a single production system rather than independent components.
Make the final decision around stable information
The best sensor is not necessarily the one with the lowest stated pressure capability or the broadest measurement range. It is the one that supplies stable, representative, and actionable information at the point where the process needs to make a decision.
Before final selection, confirm the normal working range, all gases and vapors, required control response, measurement location, signal integration, service access, and the consequence of drift. When these conditions are clear, the choice between thermal, diaphragm-based, ionization, or combined vacuum measurement becomes an engineering decision tied to process stability rather than a comparison of catalog specifications alone.