
For precision surface treatment, the phrase impact force sounds straightforward until a team tries to compare two micro-jet systems and realizes they are not really measuring the same thing. In Japan, where fine finishing, contamination control, and substrate protection are often judged very tightly in sectors such as electronics, medical components, optics, and precision machining, micro-jet impact force is rarely evaluated as a single number. It is usually treated as a process behavior: how strongly the jet acts, how consistently it acts, and whether that action removes what it should without damaging what must remain.
That is why technical evaluation needs to go beyond brochure claims. A stronger jet is not automatically better. On delicate substrates, excess force can change roughness, deform edges, drive particles into micro-features, or reduce coating adhesion later in the line. On the other hand, a jet that is too soft may look safe in testing but fail in production when contamination load shifts or part geometry becomes more complex.
What should “micro-jet impact force” mean in practice?
In practical evaluation, micro-jet impact force is not just pump pressure. It is the effective mechanical action delivered to a target surface through a specific nozzle, at a specific stand-off distance, with a specific fluid condition, spray angle, and treatment time. If any of those shift, the actual impact seen by the part shifts too.
This matters in Japan because many manufacturers and integrators tend to evaluate process windows carefully, especially when the treatment step sits upstream of bonding, coating, marking, plating, vacuum processing, or cleanliness inspection. A micro-jet cleaning or activation stage may look auxiliary on the process map, but it can influence yield as much as a more visible primary machine. That broader view is familiar across industrial support technologies, whether the issue is ultrasonic cleaning uniformity, laser marking legibility, batching accuracy, or vacuum stability.
So when reviewing micro-jet impact force Japan requirements, start by defining the process outcome, not the machine headline specification.
Start from the treatment objective, not the nozzle catalog
The most common evaluation mistake is comparing equipment by pressure range alone. Pressure helps, but it does not tell you whether the jet is intended to remove fine particles, strip a weak residual film, activate a surface before coating, or treat a patterned substrate with narrow tolerance on edge integrity.
A useful internal question set is simple:
- What exactly must be removed, modified, or preserved?
- Is the critical risk under-treatment or over-treatment?
- Does the part have flat, open access, or recessed micro-features?
- Will the next process step magnify small treatment errors?
For example, if the next step is a high-spec coating or adhesive bond, the evaluation should include not only visible cleanliness but also surface response consistency. If the next step is coding, laser marking, vacuum deposition, or electrostatic coating, local treatment variation can show up later as poor contrast, weak adhesion, pinholes, or uneven film behavior. In other words, impact force has to be judged in context of downstream sensitivity.
Why the substrate often tells you more than the machine spec
A technical evaluator usually learns more from the part than from the sales sheet. Metals, ceramics, engineering plastics, thin films, plated layers, and composite materials react differently even under similar nominal jet conditions. Surface hardness is only part of the story. Geometry, coating stack, previous machining marks, trapped contamination, and moisture behavior all influence how force is transmitted and what kind of risk appears first.
On rigid metal components, the concern may be whether the jet reaches narrow channels or removes particles from machined edges without redeposition. On softer polymers, the concern may shift to whitening, micro-scratching, localized stress, or subtle texture change that affects later inspection. With thin coatings or plated surfaces, the issue may not be immediate visible damage but cumulative instability after repeated passes.
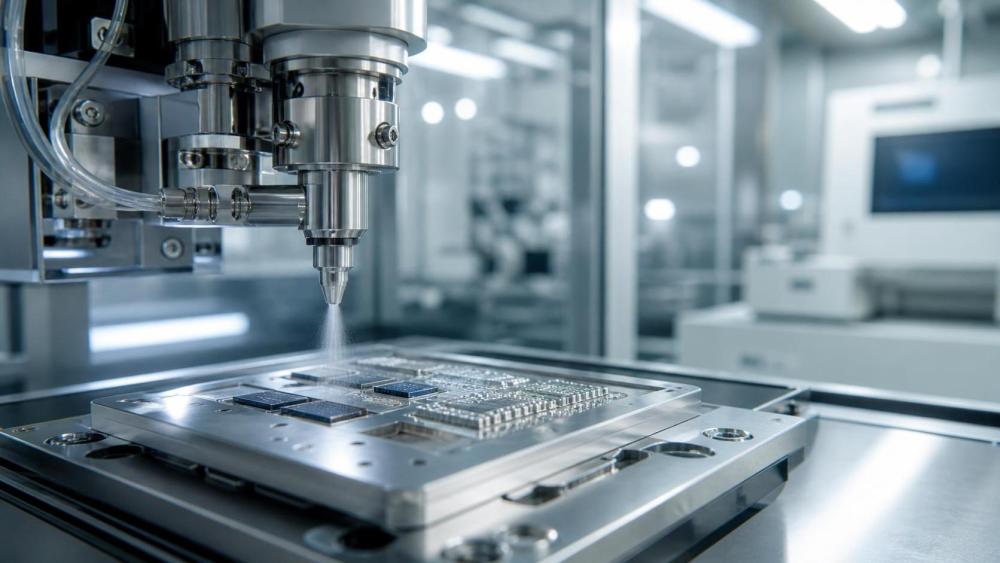
That is why a good evaluation plan usually includes pre- and post-treatment observation methods matched to the material. Depending on the application, that may mean microscopy, roughness comparison, contact angle observation, residue checks, adhesion tests, or dimensional review. No single method fits every line, and in Japan especially, acceptance criteria are often tied to the actual customer drawing, internal process standard, or product qualification route rather than to a generic impact-force claim.
Nozzle design changes the meaning of force
Two systems with similar pressure readings can behave very differently at the work surface because nozzle geometry reshapes the energy distribution. Orifice size, internal channel design, fan or point pattern, droplet formation, pulsation behavior, and flow stabilization all affect how concentrated or dispersed the impact becomes.
A narrow, concentrated jet may improve local cleaning on stubborn contamination, but it can also create a steep force gradient that makes sensitive parts harder to process consistently. A wider pattern may look gentler and cover more area, but if the target feature is deep or shielded, actual treatment effectiveness may drop even though the nominal flow rate is higher.
This is one reason comparative trials should not treat “same pressure, same time” as equal conditions. Stand-off distance and angle should be controlled carefully, and the nozzle condition itself needs attention. Wear, partial blockage, assembly tolerance, and fluid contamination can all change the delivered force profile over time. For technical teams reviewing Japanese suppliers or systems for use in Japan, repeatability of that profile may matter as much as peak force.
What to verify during measurement and validation
There is no universal shortcut measurement that fully captures micro-jet impact force across every application. Some builders rely on internal test methods, some users build application-specific fixtures, and some projects judge performance through correlated part results rather than a direct force number alone. That is not a weakness; it reflects the fact that treatment quality is interaction-based.
Still, a robust validation approach should document the variables that most often distort comparisons:
If a supplier offers force data, ask how it was measured and under what setup. If the data cannot be tied back to nozzle type, fluid condition, distance, and target material, it is hard to use that number for purchasing or qualification decisions.
The Japan-specific angle: consistency, documentation, and process discipline
When teams search for guidance on micro-jet impact force Japan, they are often not looking for a uniquely Japanese physics model. They are looking for a way to align process evaluation with Japanese manufacturing expectations: stable repetition, clear work standards, traceable parameter control, and low tolerance for avoidable variation.
In many precision manufacturing environments, especially those linked to export, regulated sectors, or tightly specified supply chains, equipment is judged not only by whether it works in a demo but by whether it can be validated, documented, and kept within control over time. That means maintenance routines, nozzle replacement intervals, calibration practices for related sensors, and operator instructions all matter. An auxiliary process step that drifts quietly can undermine an otherwise capable line.
This is also why industrial intelligence platforms such as GIAS have practical value beyond basic product browsing. In categories like surface treatment, ultrasonic systems, vacuum support, coding, and coating, the real decision is often about process fit and quality risk, not just machine type. Evaluators need comparable technical language and enough context to separate a useful specification from a decorative one.
Common misreadings during equipment comparison
A few patterns show up again and again in evaluation work.
One is assuming that visible cleanliness proves correct impact force. It may only prove that the sample was easy to clean. Another is using a robust metal test coupon to qualify a process that will later run on mixed materials or thin-feature parts. Teams also sometimes optimize for removal rate and ignore what happens after repeated cycles, especially in lines where the same fixture, holder, or product family sees long production runs.
Then there is the specification trap: a buyer asks for maximum pressure, while the production engineer really needs a controllable low-to-medium force window with tight repeatability. Those are not the same purchase criteria. If your concern is substrate safety and process consistency, turndown stability may be more important than top-end capability.
A practical evaluation path
For most projects, the cleanest approach is to narrow the question into three linked checks: can the jet achieve the intended surface effect, can it do so without creating unacceptable damage or variability, and can that condition be held consistently in production?
That usually means running controlled trials on real parts or representative coupons, defining what “pass” actually means for the next process step, and documenting the operating window in a way that manufacturing and quality teams can maintain. If local or customer-specific standards apply, those should be mapped early. If they do not, internal acceptance criteria should still be explicit enough to avoid subjective approval.
A micro-jet system that looks excellent in isolation may still be the wrong fit if its force profile is too sensitive to nozzle wear, fluid condition, or positional drift. Conversely, a less aggressive system may be the better industrial choice if it gives a wider stable window and protects downstream quality.
In the end, evaluating micro-jet impact force in Japan is less about chasing a headline number and more about proving controlled interaction between jet, material, and manufacturing intent. If that interaction is documented clearly, compared honestly, and checked against downstream risk, the equipment decision becomes much easier to defend later.