
What to Check Before Comparing a Manufacturing Compliance Technology Supplier
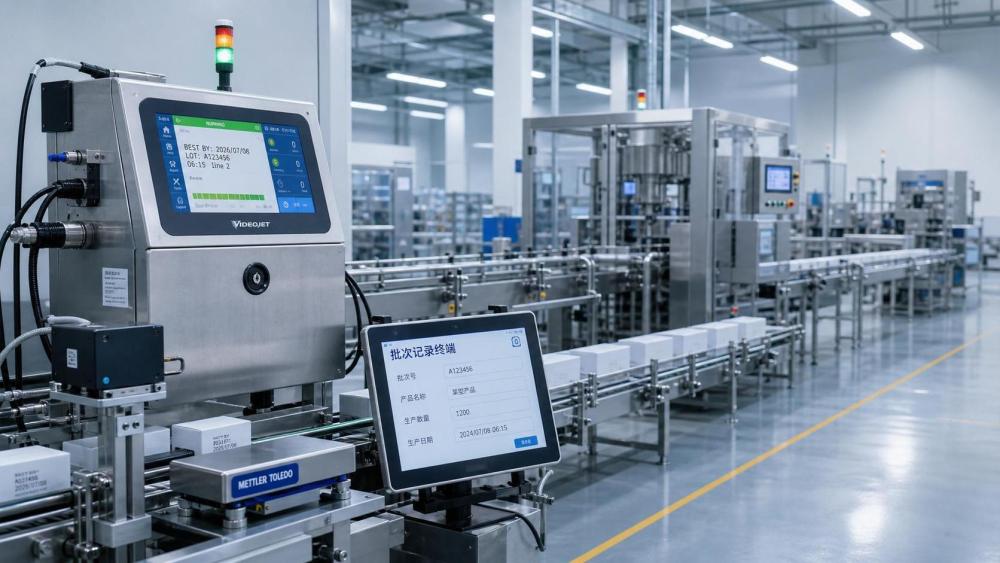
Before comparing any Manufacturing Compliance Technology supplier, pricing should not be the first filter.
A lower quote can hide weak validation support, limited documentation, or poor integration with plant systems.
That matters even more in industries where traceability, process consistency, and audit readiness shape daily operations.
A strong Manufacturing Compliance Technology supplier should help reduce risk across production, quality, and regulatory workflows.
This includes support for marking, coding, weighing, cleaning, vacuum stability, coating control, and production data visibility.
In practice, the best supplier comparison starts with operational fit, not brochure language.
Start With Regulatory Scope and Industry Fit
Every Manufacturing Compliance Technology supplier claims to understand compliance, but the real question is where that experience comes from.
A supplier serving electronics, medical devices, food processing, or battery production faces very different control requirements.
Ask which standards, audit frameworks, and customer environments the supplier supports regularly.
Look for evidence tied to real manufacturing conditions, not only generic compliance statements.
This is especially important for auxiliary systems that influence final quality without being the main production asset.
For example, ultrasonic cleaning affects contamination control, while coding systems affect product traceability and recall readiness.
A credible Manufacturing Compliance Technology supplier should explain those links clearly.
Questions worth asking early
- Which industries represent the supplier’s strongest installed base?
- What regulations or customer audit standards shape the system design?
- Can the supplier show recent examples from similar production environments?
- Are compliance features built into the product, or added later as options?
Check Traceability Depth, Not Just Basic Data Output
Traceability is often the deciding factor when comparing a Manufacturing Compliance Technology supplier.
Still, many systems only capture surface-level records.
That may be enough for simple logging, but not for investigations, export reviews, or customer complaints.
A useful traceability setup should connect process parameters, operator actions, product identifiers, batch history, and time stamps.
It should also protect data integrity and keep records searchable.
From a decision standpoint, ask whether the system supports root cause analysis, not only record retention.
For laser marking, inkjet coding, weighing, and batching systems, this depth becomes critical very quickly.
The right Manufacturing Compliance Technology supplier should be able to map data fields to actual plant workflows.
Signs of stronger traceability support
- Batch and serial-level record capture
- Audit trails for edits, overrides, and alarms
- Integration with MES, ERP, SCADA, or quality systems
- Clear retention rules and exportable records
- Support for anti-counterfeit identification where relevant
Review System Reliability Under Real Production Conditions
Compliance technology does not create value if it fails under normal factory pressure.
This is where many supplier evaluations become too theoretical.
A Manufacturing Compliance Technology supplier should show how the system performs across heat, dust, vibration, shift changes, and maintenance cycles.
Reliability should include software stability, sensor accuracy, communication uptime, and spare parts planning.
For vacuum systems, surface treatment lines, and industrial weighing equipment, small deviations can create larger compliance failures later.
More importantly, repeatability matters as much as peak performance.
A capable Manufacturing Compliance Technology supplier should provide maintenance intervals, failure history, and calibration strategy in plain terms.
Operational checkpoints to compare
- Expected uptime in comparable plants
- Calibration frequency and verification methods
- Alarm handling, fail-safe modes, and recovery steps
- Availability of local service and replacement parts
- Validation support after software updates or parameter changes
Assess Documentation Quality and Audit Readiness
Documentation quality is one of the clearest ways to judge a Manufacturing Compliance Technology supplier.
If the documents are vague, outdated, or hard to align with plant procedures, future audits become slower and more expensive.
Good documentation should support installation, operation, validation, maintenance, and change control.
It should also match what the supplier actually delivers.
In real projects, mismatched documents create avoidable compliance gaps.
That is especially true when export customers, regulated industries, or multinational facilities require standardized evidence.
A reliable Manufacturing Compliance Technology supplier should offer documentation packages that are complete and reviewable before purchase approval.
Key documents to request
- Technical specifications and system architecture
- Validation or qualification support documents
- Calibration certificates and test reports
- Change logs and software version control records
- User manuals with maintenance and troubleshooting guidance
Look Closely at Integration, Scalability, and Support Model
A Manufacturing Compliance Technology supplier may look strong on features, yet still create friction after installation.
The usual problem is poor fit with existing production systems.
That includes communication protocols, reporting formats, user permissions, and line-level data exchange.
In growing factories, another issue appears later: the system cannot scale without redesign.
A better supplier evaluation checks both present needs and future rollout potential.
This matters for multi-site operations, exporters, and teams standardizing quality controls across product lines.
A dependable Manufacturing Compliance Technology supplier should also explain response times, training coverage, and escalation paths.
Compare support beyond the sales stage
Use a Risk-Based Comparison Instead of a Feature Checklist
Feature lists are useful, but they rarely decide long-term value.
A sharper way to compare a Manufacturing Compliance Technology supplier is to score risk exposure.
Ask what happens if records are missing, calibration drifts, identification fails, or support delays interrupt production.
Then estimate the operational and commercial impact.
This approach usually reveals stronger differences than price comparison alone.
It also helps align procurement decisions with quality, compliance, and factory leadership priorities.
In current manufacturing markets, that alignment is becoming more important, not less.
The right Manufacturing Compliance Technology supplier should strengthen process control while making audits, scaling, and supplier communication easier.
Before making a final comparison, build a shortlist based on regulatory fit, traceability depth, reliability, documentation, and service capability.
That creates a more practical purchasing decision and lowers compliance risk long after commissioning.