
An industrial process standards audit is only useful when it tests whether the process can repeatedly produce conforming output, not when it merely confirms that documents exist. A calibration certificate, a signed work instruction, or a completed inspection form may be necessary evidence, but none proves that operators follow the defined method, equipment remains within control, or a nonconforming condition is contained quickly enough.
The most effective audit checklist links four things: the approved requirement, the evidence that the requirement is being met, the risk created when it is not met, and the corrective action needed to restore control. This approach is especially important for auxiliary manufacturing processes. Cleaning, coding, weighing, vacuum generation, surface preparation, and coating may sit outside the primary production machine, yet a weakness in any one of them can affect safety, traceability, product performance, or release decisions.
Start with the process requirement, not the available paperwork
A weak audit begins by asking, “What records can the department show?” A stronger audit begins with, “What must this process achieve, and what conditions make that result reliable?” The difference matters because records can be complete while the process itself has drifted away from the approved standard.
Each checkpoint should be tied to a defined process characteristic. For example, an ultrasonic cleaning stage may need to remove specified contamination without damaging a precision part. A batching operation may need to add materials in the correct sequence and quantity. A laser mark may need to remain readable after downstream handling. A vacuum system may need to maintain stable operating conditions long enough for a coating, packaging, degassing, or drying cycle to work as intended.
For every critical characteristic, the audit should identify:
- the approved specification, work instruction, control plan, or customer requirement;
- the process setting, material condition, equipment state, or operator action that controls it;
- the objective evidence that confirms the control was applied;
- the method for detecting loss of control;
- the containment and escalation action when the requirement is not met.
This structure prevents a common mistake: treating the quality system as separate from the production process. In practice, the audit should show how a written requirement becomes a controlled operating condition, how that condition is verified, and what happens when verification fails.
Evidence that should withstand an audit
Evidence is more than a file attached to an audit report. It should be current, traceable to the process being examined, understandable to the person using it, and capable of showing whether the requirement was met at the relevant time. A document that is technically approved but unavailable at the workstation is weaker evidence than an accessible, controlled instruction that matches the actual operation.
The audit does not need to request every record ever created. Sampling is more valuable when it follows risk. Select recent production runs, different shifts, a changeover, an equipment alarm, a maintenance event, or a batch with an unusual result. These points reveal whether the process remains controlled under normal variation rather than only during a prepared audit demonstration.
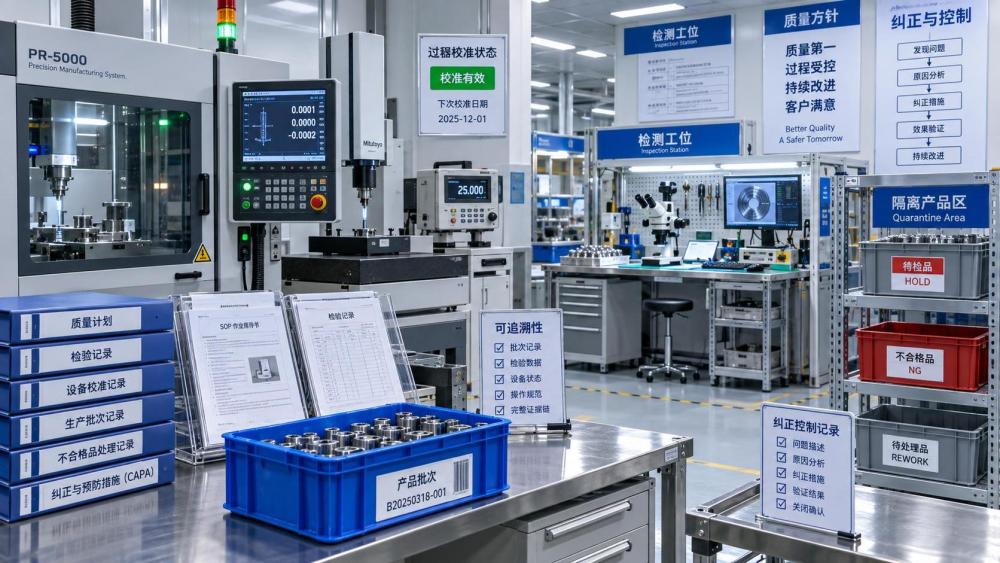
Audit the point where control can be lost
Many process failures begin at interfaces: after maintenance, during product changeover, when materials are replenished, after a software update, or when an operator responds to an alarm. A checklist that focuses only on stable running conditions can miss the moments when unauthorized settings, wrong materials, incomplete cleaning, or incorrect records enter the process.
Cleaning and ultrasonic processing
For cleaning operations, assess the full cleaning system rather than the tank alone. Review the defined loading method, fixture condition, solution preparation, filtration or replenishment practice, rinse quality, drying method, and inspection criteria. A clean-looking part is not always a conforming part. If the process protects bonding, coating adhesion, sealing, welding, or precision assembly, the acceptance method must be appropriate to that downstream risk.
Look for evidence that bath condition is monitored according to the process need and that parts cannot bypass the required cycle. Also examine what happens after a failed or interrupted cycle. Re-running a part may be acceptable in some processes, but it should not become an informal habit without a defined decision rule, because repeated exposure can introduce damage, redeposition, or uncertainty about the part’s history.
Weighing and batching
In weighing and batching, the central question is not simply whether scales have been calibrated. The checklist should verify recipe version control, material identity, lot traceability, weighing sequence, tolerance handling, reconciliation, and the disposition of an out-of-tolerance addition. A scale can be accurate while the batch is wrong because an operator selected the incorrect recipe, scanned the wrong material, or accepted a result outside the approved range.
Electronic records can improve traceability, but they should be checked for practical control: who can alter a recipe, whether changes are reviewed, whether an interrupted batch is clearly identified, and whether manual additions are documented with the same discipline as automated ones. Where manual intervention is permitted, the instruction should define the trigger, authorization, record, and verification required.
Traceability marking and coding
For laser marking and inkjet coding, audit both the content and the durability of the mark. The correct serial number or batch code has little value if the mark becomes unreadable, is placed on the wrong surface, or cannot be associated with the production record. Confirm how data are generated, transferred, verified, and protected from duplication or manual entry error.
Inspect the first-off check, periodic verification, and response to poor legibility. A simple visual check may be sufficient for a clearly visible code, but a more demanding application may require verification of contrast, placement, permanence, or machine-readable content. The audit should also trace a finished item backward through the mark to the relevant production, material, and inspection records.
Vacuum, surface treatment, and coating
Vacuum-related process control should address more than the displayed pressure value. Review leak checks, pump maintenance, filter or fluid condition where applicable, sensor verification, alarm response, and the defined recovery action after an interruption. Vacuum instability can change drying, degassing, packaging integrity, deposition, or coating conditions even when the final display appears normal at the end of the cycle.
For surface treatment and electrostatic coating, focus on preparation, environmental conditions, application settings, grounding or electrical controls where relevant, cure or post-treatment requirements, and inspection of the finished surface. A finished part may appear acceptable at release while still carrying a risk of poor adhesion, inconsistent coverage, corrosion exposure, or downstream assembly problems. The audit needs to connect preparation evidence and process settings to the acceptance criteria for the completed surface.
Use a checklist that distinguishes observation from proof
A useful industrial process standards audit checklist does not allow “yes” to become a substitute for evidence. Each item should prompt the auditor to record what was reviewed, what was observed, which record or sample was checked, and whether the evidence supports the stated requirement.
For example, “Operator trained” is too broad. A better checkpoint is: “The assigned operator is authorized for the current process revision, can locate the applicable instruction, and can explain the action required when the monitored value exceeds its limit.” This tests authorization, document availability, understanding, and response capability in one observation.
Similarly, “Equipment maintained” should become: “Preventive maintenance and corrective repairs are recorded; overdue work is evaluated for product impact; and the machine condition observed at the time of audit is consistent with its intended operation.” The goal is not to make the checklist longer. It is to remove vague items that can be closed without meaningful verification.
Corrective actions should repair the control system
A correction fixes the immediate condition. A corrective action addresses why the condition could occur and why existing controls did not prevent or detect it. Confusing the two produces repetitive audit findings: a record is completed after the fact, a label is replaced, a setting is restored, and the same weakness returns at the next shift or next production run.
When a nonconformance is found, first contain the possible impact. Identify affected product, batches, equipment status, and records. Stop further release when the available evidence cannot demonstrate conformance. Containment should be proportionate to the risk, but it must be clear enough that suspect material cannot be confused with accepted output.
Then investigate the control failure. Ask whether the requirement was unclear, the instruction was impractical, training did not cover the real decision point, maintenance was not linked to product risk, monitoring was too infrequent, or the acceptance method could not reveal the failure. Operator error may describe the final event, but it rarely explains why the system allowed the event to pass.
A robust corrective-action record normally includes the affected requirement, evidence reviewed, immediate containment, root cause, action owner, completion date, and effectiveness check. The effectiveness check should test the actual failure path. If a wrong recipe was selected during changeover, reviewing a newly signed training sheet is not enough. The better test is to observe a later changeover, confirm access controls and verification steps, and verify that the revised method prevents selection of an unauthorized recipe.
Common audit findings that deserve closer scrutiny
- Signed records with missing process context: A value is recorded, but there is no product, batch, equipment, or time reference that makes the record traceable.
- Calibration treated as complete process control: The instrument is calibrated, but the measurement method, sampling point, or reaction plan is not adequate.
- Old instructions at the point of use: The controlled master is current, while an obsolete printout or local file directs the actual work.
- Temporary deviations that become routine: Workarounds for alarms, missing materials, or equipment downtime are repeatedly used without formal review.
- Corrective actions closed on completion rather than effectiveness: The task is marked complete without evidence that recurrence risk has been reduced.
- Weak linkage between upstream and downstream checks: A coating defect, unreadable mark, or contamination issue is identified at final inspection, but the related process controls are never reassessed.
Set the audit scope around risk and change
Not every process requires the same depth of review. A low-risk visual handling step may need basic instruction control and supervision. A process that affects product identity, chemical composition, cleanability, pressure integrity, surface performance, or worker exposure requires tighter evidence and a more deliberate response plan. The appropriate level of control depends on what can fail, how quickly failure can be detected, and whether the result can be corrected before release.
Changes should automatically raise the audit priority. New materials, revised recipes, replacement pumps, altered cleaning chemistry, new marking data sources, modified fixtures, or changed coating parameters can invalidate assumptions built into existing records. The question is not whether the process still looks familiar. It is whether the defined controls still match the current process.
Resources such as Global General Industrial Auxiliary Systems can help teams compare the operating considerations behind ultrasonic cleaning, marking, batching, vacuum, and surface-treatment systems. That comparison is most useful when it supports a specific audit question: what must be controlled, what evidence should exist, and what failure mode the chosen equipment or process arrangement needs to prevent.
Make the next audit actionable
Before beginning the next review, select the process characteristic with the greatest consequence if it drifts: an incorrect batch addition, incomplete cleaning, lost traceability, vacuum loss, or insufficient coating protection. Trace that characteristic from the approved requirement to the operator’s action, the machine setting, the supporting record, the inspection result, and the response to an abnormal condition.
If the chain is complete and consistent, the process is likely being managed as a system. If one link depends on memory, an undocumented workaround, or a record that cannot be connected to the product, the audit has identified where corrective action should begin.