
Industrial process certification USA requirements can directly influence product quality, worker safety, traceability, and market access. For quality control and safety managers, a successful audit is rarely the result of a well-written manual alone. It comes from proving that cleaning, marking, batching, vacuum, coating, and related support processes remain under control on an ordinary production day—not only when an auditor is walking the floor.
This distinction matters. In advanced manufacturing, auxiliary systems often sit outside the spotlight of the primary machine, yet they can determine whether a part is clean enough to assemble, whether a batch contains the correct formulation, whether a safety-critical component can be traced, or whether a coating meets durability and environmental expectations. A missed calibration, an uncontrolled recipe edit, or an unreadable product code can become the evidence an auditor follows back to a larger system failure.
For manufacturers searching for industrial process certification USA guidance, the first practical point is that the United States does not issue one universal “industrial process certificate.” Requirements depend on the product, market, customer contracts, workplace risks, and applicable federal, state, or local rules. Many companies must combine a recognized management-system certification with regulatory compliance, customer-specific audit criteria, and equipment-validation evidence.
Start by separating certification, regulation, and customer approval
Audit preparation becomes much clearer when the compliance landscape is divided into three layers.
- Management-system certification commonly includes ISO 9001 for quality management, ISO 14001 for environmental management, and ISO 45001 for occupational health and safety. These certifications are generally voluntary, but major customers, exporters, and supply-chain partners may require them.
- Regulatory obligations are mandatory where they apply. OSHA requirements govern workplace safety. EPA-related obligations may affect emissions, wastewater, hazardous materials, and coating operations. FDA requirements can be central in food, pharmaceutical, medical-device, and certain cosmetic manufacturing. Additional state rules may be more restrictive than federal baselines.
- Customer, industry, or third-party approvals may include supplier audits, automotive quality requirements, aerospace special-process controls, UL-related product expectations, or buyer-specific process validation standards.
Confusion between these layers creates a common audit weakness. A site may hold ISO 9001 certification while still failing a customer audit because its laser-marking verification is inconsistent. Another facility may meet a buyer’s quality requirements but lack evidence that chemical handling, ventilation, or lockout/tagout practices meet applicable safety obligations. Certification is important, but it is not a blanket exemption from regulatory or contractual duties.
What auditors are actually trying to establish
Auditors do not simply check whether policies exist. They test whether the documented system matches reality. In a process-focused audit, the underlying questions are usually straightforward:
- Is the process defined, including acceptable limits and responsibilities?
- Are operators using the current approved instructions?
- Can the site demonstrate that critical equipment is suitable and maintained?
- Are measurement results reliable, traceable, and reviewed?
- When something goes wrong, is the nonconforming output contained and investigated?
- Can management show that corrective actions were completed and remained effective?
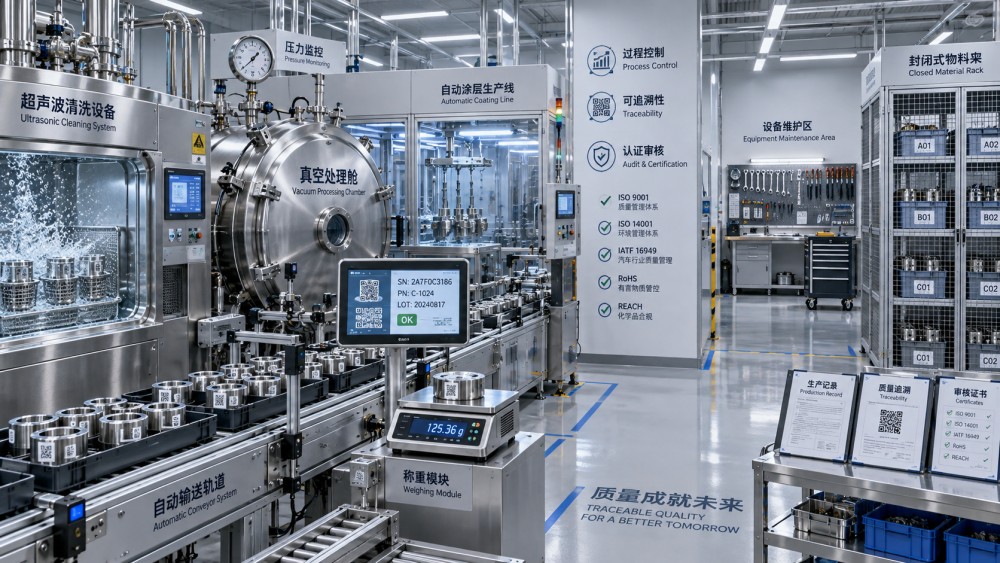
A convincing answer requires connected evidence. An approved ultrasonic cleaning procedure, for example, should align with the actual tank settings, solution concentration records, temperature controls, maintenance logs, operator training, part-handling method, and cleanliness-verification results. If these pieces tell different stories, an auditor will see a process that is documented but not controlled.
Build the audit trail around critical process parameters
The most useful audit files are not necessarily the thickest. They make it easy to follow a product or batch from incoming material to release. Quality and safety teams should identify the variables that can change the output, define allowable ranges, decide how they will be monitored, and preserve evidence of review.
For an industrial weighing and batching system, critical parameters may include ingredient identity, lot number, target weight, scale tolerance, dispensing sequence, mixing time, and recipe revision. For vacuum-assisted processing, they may include pressure level, leak rate, evacuation time, temperature, pump maintenance status, and alarm response. In coating operations, key controls often extend to surface preparation, powder or liquid material lot, film thickness, curing profile, booth airflow, grounding, and inspection criteria.
Not every machine setting needs the same level of control. The important task is to distinguish a convenience setting from a parameter that can affect safety, performance, compliance, or customer requirements. A risk-based review—often supported by process FMEA, hazard analysis, or a similar method—helps teams focus records where audit scrutiny is most likely.
Cleaning systems: prove that “clean” has a measurable meaning
Ultrasonic cleaning is frequently treated as a routine utility process until contamination causes adhesion failure, assembly defects, coating problems, or early product failure. Auditors may ask how the manufacturer defines cleanliness and why the chosen verification method is appropriate for the component.
Depending on the application, evidence may include bath concentration checks, solution replacement schedules, temperature and cycle-time records, ultrasonic performance checks, water-quality controls, particle or residue testing, drying controls, and protected handling after cleaning. The method should be proportionate to the risk. A general industrial component and a precision medical or semiconductor-related part will not require the same verification approach, but both require a defensible rationale.
Marking and coding: traceability must survive the real world
Laser marking and inkjet coding support lot control, anti-counterfeiting, warranty analysis, and recall readiness. Their audit value depends on legibility and data integrity, not merely on the existence of a code.
Keep records showing the approved code format, data source, software access controls, artwork or template revision status, first-piece verification, and routine readability checks. Where codes are scanned downstream, demonstrate that the scanner, database, and physical mark work together. If a code links to a production batch, the batch record should allow a reviewer to identify the relevant materials, equipment, operators, and inspection status without relying on memory.
Vacuum and coating processes: document the conditions behind the finish
Vacuum performance can affect degassing, packaging integrity, coating adhesion, freeze-drying consistency, and semiconductor-related operations. A pressure reading alone may not prove process capability. Auditors may look for gauge calibration, leak-testing practices, alarm set points, preventive maintenance, filter changes, pump-fluid controls, and contingency steps when a cycle aborts.
Surface treatment and electrostatic coating bring another layer of risk. The final appearance may look acceptable while corrosion resistance, adhesion, cure, or coverage is inadequate. Control plans should connect pre-treatment checks, material identification, grounding, environmental conditions, application settings, oven profiles where relevant, film-thickness measurements, and defect disposition. Environmental and worker-safety obligations also deserve attention: chemical storage, ventilation, combustible dust considerations, waste handling, and personal protective equipment cannot be separated from process quality.
Calibration records are necessary, but measurement discipline is broader
During a certification audit, missing calibration stickers are easy to notice. More subtle issues can be more damaging: a calibrated scale used outside its intended range, a pressure gauge with no defined acceptance tolerance, a test method performed differently by each shift, or a spreadsheet that permits uncontrolled edits.
For each measurement that supports a release decision or verifies a critical parameter, establish the instrument identity, calibration interval, traceability route, allowable error, handling requirements, and action to take when equipment is found out of tolerance. If a device fails calibration, the team should assess whether prior measurements and potentially released product were affected. Simply replacing the instrument does not close the quality question.
Equally important is measurement system capability. A coating-thickness gauge, barcode verifier, temperature probe, or weighing scale may be calibrated and still produce inconsistent decisions if operators use it differently or the method is poorly defined. Clear work instructions, repeatability checks, competency confirmation, and controlled data capture reduce this gap.
Safety evidence should be visible on the production floor
Quality managers sometimes treat safety documentation as a separate department’s responsibility. In practice, process audits often expose the connection. An improperly guarded ultrasonic welding station, a vacuum chamber without an adequate maintenance procedure, a coating booth with poor housekeeping, or an emergency response plan that no one has practiced can affect both people and operational continuity.
For US manufacturing facilities, relevant OSHA expectations may involve hazard communication, machine guarding, lockout/tagout, electrical safety, respiratory protection, hearing conservation, powered industrial trucks, confined-space risks, and recordkeeping. The applicable scope depends on the facility and process. Safety managers should ensure that risk assessments are reflected in actual controls: labeled chemicals, accessible safety data sheets, current training records, usable PPE, inspection routines, and documented incident or near-miss follow-up.
An auditor may ask an operator what happens when an alarm occurs or when a machine needs servicing. That answer often reveals more than a signed training roster. Training should be role-specific, refreshed after procedural changes, and supported by observation or practical competency checks where the task carries meaningful risk.
The audit-ready record set: less hunting, more evidence
When an auditor requests a production record, the worst outcome is a long search through disconnected folders, paper binders, personal spreadsheets, and machine screens. A controlled document system does not need to be expensive or complex, but it must make current information identifiable and obsolete versions unavailable for routine use.
A practical audit package normally includes:
- Process maps, control plans, risk assessments, and approved work instructions;
- Equipment qualification, preventive maintenance, and repair histories;
- Calibration and verification records for critical instruments;
- Batch records, cleaning logs, recipe records, marking-verification data, or coating-inspection results as applicable;
- Supplier qualification and incoming-material controls for critical consumables;
- Training and authorization records;
- Internal audit findings, corrective-action reports, and effectiveness reviews;
- Management-review evidence showing that quality and safety performance are actively evaluated.
Electronic records can strengthen traceability, particularly when process equipment automatically captures settings, alarms, and timestamps. Yet digital systems introduce their own audit questions: Who can change a recipe? Are changes logged? Can data be overwritten? Is there a backup and retention policy? Access control and electronic data integrity should be considered early rather than added after a customer raises concerns.
Internal audits should follow the product, not just the checklist
A clause-by-clause internal audit is useful, but it can miss the experience of an actual product moving through the plant. A stronger method is to select a completed order, batch, or serialized component and trace it backward and forward. Review the purchase information, incoming inspection, process settings, operator authorization, inspection results, nonconformance history, packaging, and shipment record.
This approach exposes disconnected controls quickly. Perhaps the batch record lists a material lot that procurement cannot verify. Perhaps the laser code shows a date that does not match the production record. Perhaps a coating thickness result is present, but the gauge’s calibration had expired. These are not merely paperwork defects; they are signals that traceability and decision-making may be unreliable.
Audit findings should lead to root-cause analysis rather than cosmetic correction. Replacing a missing form may address the symptom. The deeper issue could be an unclear ownership model, an impractical record format, insufficient operator training, or a process change that never reached the floor.
Common certification audit mistakes in industrial support processes
Several patterns appear repeatedly across manufacturing environments:
- Documenting ideal conditions instead of actual operations. Procedures say one thing; experienced operators use a different, unofficial method.
- Controlling the primary process but ignoring the auxiliary step. Cleaning, marking, vacuum generation, weighing, and surface preparation are treated as low-risk despite their direct effect on final quality.
- Using preventive maintenance as proof of process validation. Maintenance keeps equipment available; it does not by itself demonstrate that the output meets requirements.
- Closing corrective actions too quickly. A completed action without effectiveness evidence is vulnerable during surveillance or customer audits.
- Assuming one certification covers every market need. A quality-management certificate may support credibility, but sector regulations and customer specifications still apply.
Making industrial process certification a continuing control system
The most resilient manufacturers do not prepare for audits as isolated events. They use audits to test whether their process knowledge is still valid as equipment, personnel, materials, suppliers, and customer expectations change. This is particularly valuable for factories relying on auxiliary technologies, where small variations can quietly affect cleanliness, identification, dosage, pressure stability, or protective finish quality.
For quality control and safety leaders, the next step is practical: map the critical support processes, identify the evidence that proves each one is controlled, and walk that evidence against what happens on the floor. Where the two do not match, the gap is already visible—before an external auditor, customer, or product failure makes it urgent.
A disciplined industrial process certification USA strategy is therefore not about collecting certificates for display. It is about creating repeatable conditions, trustworthy records, safer work, and traceable decisions that can stand up to scrutiny when it matters most.