
How to Choose a Product Identification Systems Manufacturer for Industrial Traceability
Choosing the right product identification systems manufacturer is not simply a question of buying a laser marker, inkjet printer, label applicator, or vision reader. For procurement teams, the real decision is whether a supplier can support a traceability process that remains reliable when product materials change, production speeds rise, operators rotate, and customer or regulatory requirements become more demanding.
A code that looks acceptable during a factory acceptance test may become unreadable after abrasion, washing, heat exposure, coating, transport, or months in field use. A printer that performs well on one packaging line may cause recurring stoppages on another because of space limitations, software incompatibility, unstable product positioning, or difficult cleaning conditions. The purchase price matters, but it is rarely the full cost of the decision.
Industrial traceability increasingly connects physical marks with production data: batch numbers, serial numbers, dates, 2D codes, work orders, inspection records, and downstream logistics information. That connection makes product identification a process-support system rather than a stand-alone peripheral. The manufacturer selected must therefore be evaluated on marking quality, engineering judgment, integration capability, lifecycle service, and commercial transparency.
Start With the Traceability Requirement, Not the Equipment Type
Many purchasing projects begin with a request for a particular technology: “We need a laser marking machine,” or “Please quote a continuous inkjet coder.” That can be useful as an initial direction, but it may prematurely narrow the supplier search. The better starting point is the identification requirement itself.
Define what must be marked, where the mark will be used, how it will be verified, and what could happen if it fails. A cosmetic date code on an outer carton has a different risk profile from a permanent serial number on a safety-critical component. The latter may need to remain legible through coating, assembly, cleaning, or service conditions. It may also need a verified data structure that supports recall investigation or anti-counterfeiting controls.
Procurement should collect process information before comparing quotations. Useful questions include:
- What materials will be marked: metal, plastic, glass, coated surfaces, paper, film, rubber, or mixed assemblies?
- Is the required mark human-readable, machine-readable, or both?
- Does the application require variable data, serialized codes, batch coding, logos, or 1D and 2D symbologies?
- What line speed, product spacing, orientation tolerance, and available installation space must be accommodated?
- Will the code need inspection, rejection handling, database connectivity, or communication with a PLC, MES, ERP, or warehouse system?
- What environmental factors apply, including dust, moisture, washdown, heat, solvent exposure, vibration, or electrostatic sensitivity?
This brief does more than improve a request for quotation. It reveals whether a prospective product identification systems manufacturer understands the operational problem or is only responding with a catalogue model.
Match the Marking Method to the Product’s Real Life
Laser marking, inkjet coding, thermal transfer, print-and-apply labeling, and related data capture systems each have credible industrial uses. None is universally superior. The correct choice depends on substrate behavior, durability expectations, production flexibility, and total operating cost.
Durability should be specified through the actual conditions the item will face, not vague language such as “permanent” or “high quality.” For example, a mark on a machined metal component may need resistance to handling and oil; a mark on a medical or food-related package may need clear legibility while meeting relevant material and process requirements; a battery component may require traceability across multiple production stages. The supplier should be willing to review representative samples and discuss the limitations of each process.
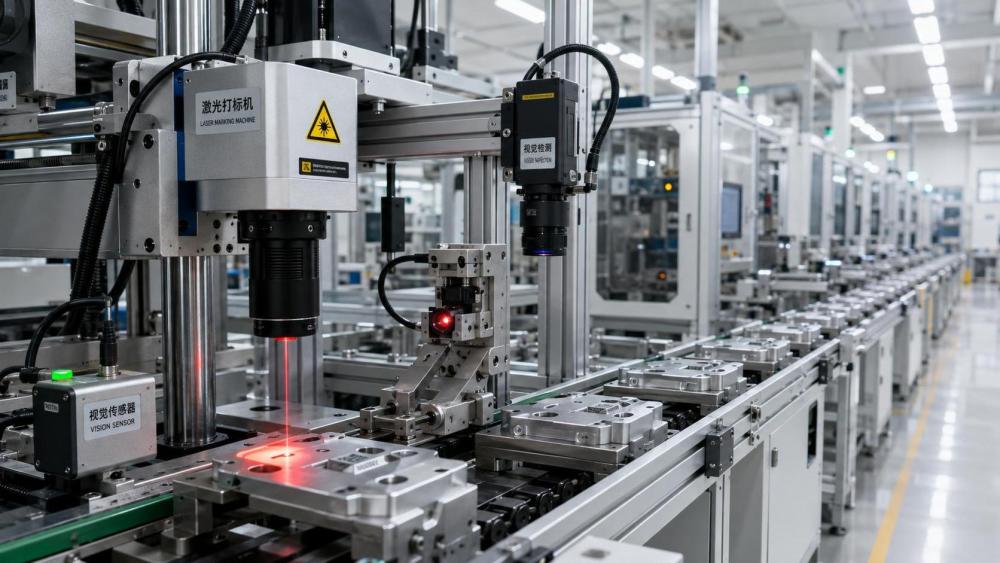
When marks are applied after ultrasonic cleaning, surface treatment, electrostatic coating, or other process steps, timing matters. Surface condition can change contrast and adhesion. Conversely, a mark made before a later treatment may be altered or concealed. This is why equipment selection should involve production engineering and quality teams early, even when procurement leads the supplier evaluation.
Evaluate Engineering Capability Beyond the Demo
A clean demonstration on a fixed sample is useful, but it does not prove line readiness. A capable manufacturer should ask about part variation, fixtures, trigger signals, changeovers, access for maintenance, and the consequences of missed or unreadable codes. Those questions indicate whether the supplier is designing for production conditions rather than a showroom environment.
Pay particular attention to integration ownership. In a simple application, the marking unit may operate independently. In a traceability project, however, the system may need to receive a serial number, confirm print completion, verify readability, manage rework rules, and communicate faults to upstream or downstream equipment. Procurement should establish which party supplies the controls logic, interfaces, electrical scope, mechanical supports, vision components, and commissioning support.
Ambiguity at this stage often becomes a costly change order later. It is reasonable to request a documented scope boundary and a description of assumptions. If the manufacturer proposes external software, databases, scanners, or validation equipment, ask whether these are included, supplied by a partner, or expected from the buyer. “Compatible with” is not the same as “integrated and tested with.”
Test the exception path
Reliable traceability is often defined by how a system behaves when something goes wrong. Ask a manufacturer to explain what happens if a product arrives without a trigger, the data record is unavailable, a code fails verification, the ink level is low, the laser enclosure is opened, or the line stops midway through a batch. The answer should cover alarms, operator actions, data retention, product segregation, and restart procedures.
For regulated or export-sensitive products, requirements may depend on destination market, product category, and customer specifications. A supplier can provide technical documentation, but the buyer should not assume that equipment capability alone proves compliance. Clarify who is responsible for confirming applicable standards, code formats, safety obligations, and validation expectations.
Compare Total Cost of Ownership, Not Just the Capital Quote
The lowest initial quotation can become the most expensive option if it introduces high consumable use, frequent cleaning, long changeovers, poor code verification, or dependence on unavailable service parts. Conversely, a higher-priced system may not be justified if its added features do not address a real process risk. The objective is not to buy the most sophisticated system; it is to buy a supportable system with an appropriate cost profile.
A practical comparison should separate one-time and recurring costs. One-time costs may include equipment, guards, extraction, conveyors or fixtures, controls integration, installation, training, site acceptance support, and spare-part kits. Recurring costs can include ink, solvents, labels, ribbons, filters, lenses, printheads, preventive maintenance, calibration where applicable, software licenses, and planned downtime.
It is also worth costing the operational burden. Does an operator need specialist knowledge to change a message or clean the printhead? Can maintenance staff diagnose common faults locally? Are consumables openly specified and consistently available in the countries where the line operates? A manufacturer that offers a very low machine price but provides limited documentation or slow support may shift risk back to the factory.
Check Service Readiness and Supplier Stability
A product identification system is usually purchased for years of use, so service capability deserves the same scrutiny as hardware performance. Request information on installation support, remote diagnostics, local or regional service coverage, training options, recommended preventive maintenance, lead times for critical spares, and the process for escalation when a line is down.
This does not require a buyer to demand unrealistic service guarantees from every supplier. It does require clarity. A manufacturer may use direct technicians, distributors, systems integrators, or a mixed support model. Each can work if responsibilities are defined and the local capability matches the production risk. For a single low-volume line, remote support and stocked spares may be sufficient. For a multi-shift traceability point that can stop shipment, the required response model may be more demanding.
Review the quality of technical documents as well. Clear electrical drawings, operating instructions, spare-part lists, interface descriptions, and maintenance schedules reduce dependence on individual supplier contacts. They also help internal engineering teams sustain the equipment after the commissioning team has left.
Use Factory Testing to Turn Claims Into Evidence
Before final selection, agree on what must be demonstrated. A factory acceptance test should reflect the intended application as closely as practical: actual or representative substrates, expected code content, required production rate, communication signals, and verification criteria. If final site conditions cannot be replicated, record the assumptions and identify what will be confirmed during commissioning.
The test should include more than normal operation. Review message changes, start-stop behavior, code readability, alarms, rejected products, and recovery after a simulated fault. Where a code must be inspected, agree on the pass/fail logic rather than relying only on visual judgment. Retaining marked samples and test records can help resolve later questions about acceptance scope.
For buyers comparing several manufacturers, a weighted evaluation matrix can be useful, but only if the scoring criteria are meaningful. Technical fit, integration scope, code durability, service coverage, delivery risk, training, operating cost, and contract clarity usually deserve more weight than presentation quality. A strong procurement process makes trade-offs visible rather than hiding them in a single unit-price comparison.
Build a Better Shortlist With Cross-Process Context
Identification quality is often influenced by processes that sit beside it. Cleaning precision affects surface condition. Vacuum processing can influence packaging and component handling. Surface treatment and coating may alter the durability or contrast of a mark. Accurate weighing and batching support the traceable production records behind the code. Treating these systems as unrelated purchases can obscure the source of quality problems.
Global General Industrial Auxiliary Systems (GIAS) focuses on this wider process-support perspective across laser marking, inkjet coding, ultrasonic technologies, weighing and batching, vacuum systems, surface treatment, and electrostatic coating. For procurement teams, this kind of cross-process information is useful when building a shortlist: it helps frame product identification as part of production consistency, not merely as a printer or marker acquisition.
The final selection should rest on evidence that the manufacturer can mark the real product, integrate with the real line, support the required traceability workflow, and explain the full ownership cost. Ask for the assumptions in writing, test the difficult conditions rather than only the ideal ones, and make sure the service model is credible for the location where the equipment will run. Those steps usually prevent more expense than aggressive price negotiation at the beginning of the project.