
A traceable production system is only as reliable as the process evidence it can preserve when something goes wrong. A serial number on a finished product may identify a unit, but it does not prove that the correct material was used, that the batch was mixed within tolerance, that a critical surface was cleaned, or that a vacuum-dependent process remained stable. For quality and safety teams, an industrial quality assurance system must connect those events into a usable chain of evidence.
The practical objective is straightforward: for any finished lot, shipment, or individual unit, the manufacturer should be able to reconstruct what was made, from which inputs, on which equipment, under which approved conditions, by whom, and with what inspection result. The same system should work in reverse. When a supplier material lot, process deviation, or customer complaint is identified, the team should be able to determine the affected product population without placing unaffected inventory on hold.
Building that capability does not begin with selecting a software platform or adding more inspection points. It begins by identifying where product integrity can be lost and deciding which conditions must be recorded, controlled, or verified before production can continue.
Start with the decisions traceability must support
Many traceability programs fail because they collect data before defining the decisions that data must enable. The result is often a large volume of timestamps, operator entries, and machine records that cannot answer a containment question quickly. A useful system is designed around a small number of operational questions:
- Which incoming material lots were used in a specific finished batch or serialized product?
- Which products passed through a machine during a parameter excursion, maintenance event, or calibration lapse?
- Was a critical process completed within its approved operating window?
- Which inspection result released the product for the next process step or shipment?
- Can the organization isolate affected stock by location, customer shipment, production date, and product identifier?
These questions should be written before deciding where to scan a code, where to install a sensor, or which records to digitize. They expose the difference between identification and traceability. Identification answers “what is this item?” Traceability answers “what happened to it?” Quality assurance needs both, but the second is where recall readiness, root-cause analysis, and defensible release decisions are established.
The required depth depends on the product and the risk. A high-volume packaged product may need lot-level genealogy, while a safety-critical component may require unit-level history. A chemical blend, food formulation, pharmaceutical intermediate, or battery material may need continuous linkage between material lots, weighing records, process conditions, retained samples, and final release. There is no benefit in imposing unit serialization on every low-risk component if the production process cannot maintain that level of control. Equally, lot-level records are inadequate when a single unit can be repaired, reworked, or exposed to a critical process independently of its batch.
Map the process around points where quality can change
A process map for traceable production should focus on transformation and risk, rather than simply mirroring the factory layout. The map needs to show where material is received, identified, stored, issued, combined, transformed, inspected, reworked, packaged, and dispatched. At each point, the team should ask three questions: what could change the product, how would that change be detected, and what record would prove the decision taken?
Auxiliary systems deserve particular attention because they frequently control conditions that are invisible in the finished product. A precision part may appear acceptable after assembly even though a cleaning stage left residual contamination that later affects adhesion, sealing, electrical performance, or corrosion resistance. A coded package may look correct while the mark is incomplete, unreadable, or linked to the wrong production record. A coating may have the right appearance despite poor surface preparation or unstable powder application. These are not peripheral details when the final failure mechanism begins upstream.
For each critical operation, define a traceability event with five elements:
- Object: the material lot, container, work order, unit, carrier, or pallet being processed.
- Operation: the approved step being performed, including the equipment or work cell.
- Conditions: the parameters that determine whether the step was acceptable.
- Result: the pass, fail, hold, measurement, or inspection disposition.
- Accountability: the operator, automated system, supervisor, or release authority associated with the event.
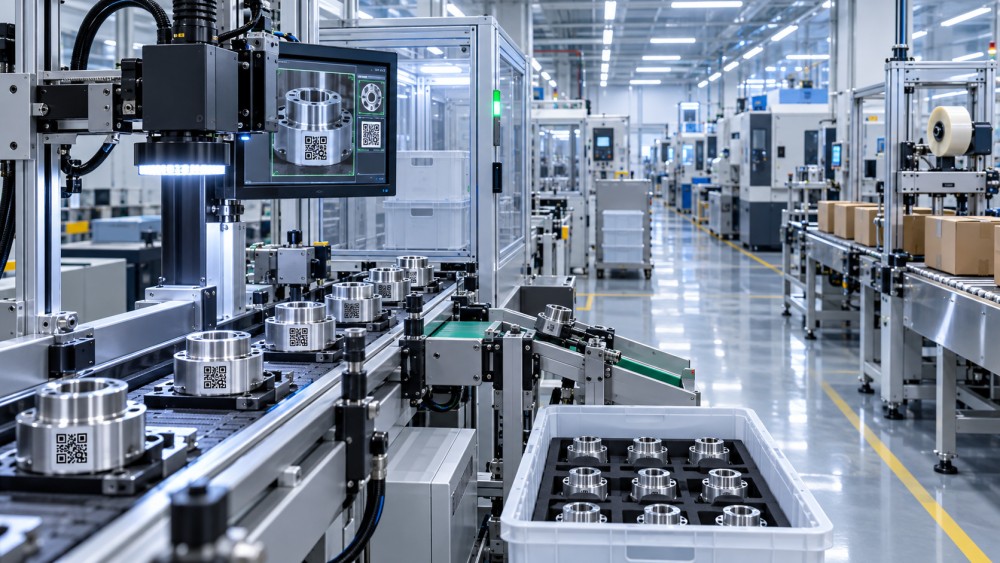
This structure avoids a common weakness: recording that a part entered a process without recording whether the process was actually capable of producing an acceptable result. For a weighing and batching operation, the record may need ingredient lot, target quantity, actual quantity, scale status, sequence, and batch identity. For vacuum processing, it may include recipe version, achieved pressure condition, hold time, alarm status, and chamber or pump identification. For laser marking or inkjet coding, it may include the code content, verification result, machine status, and the relationship between the printed or marked code and the production record.
Not every parameter should become a release record. Teams should separate values that are useful for engineering optimization from values that are necessary to prove product conformity. Over-recording creates review burdens and makes exceptions harder to see. Under-recording leaves the organization unable to establish the boundary of a deviation. The right record is the one that supports a specific quality decision, investigation, or containment action.
Control the handoffs that break product genealogy
Most gaps in traceability occur at handoffs: receiving to storage, storage to production, batch preparation to filling, cleaning to assembly, production to rework, and finished goods to shipment. These transitions are often handled through paper travelers, manual relabeling, shared containers, or informal operator knowledge. A system can have excellent equipment data and still lose its value when materials are decanted into an unlabelled container or when two lots are staged together without a controlled identity transfer.
Each handoff needs a defined rule for identity preservation. Containers, work-in-process racks, carriers, and mixed batches should carry an identifier that remains linked to the relevant source material and production context. When materials are split, merged, repacked, or reworked, the relationship must be recorded rather than overwritten. A new internal label can be created, but it should not erase the source lot or original process history.
Rework is especially important. Treating reworked material as though it had followed the original route can hide the very condition that later needs investigation. The record should show why the product was removed from normal flow, the inspection or defect code that triggered the decision, the approved rework instruction, the material identity before and after rework, and the disposition following reinspection. Where rework changes a critical characteristic, the quality plan may require a new lot definition or additional release checks.
Manual data entry remains necessary in many factories, particularly where legacy equipment is used. The aim is not to eliminate every manual step. It is to ensure that manual entries are limited to decisions a person is qualified to make and protected against predictable errors. Barcode or machine-readable code capture can reduce transcription mistakes, but scanning alone does not guarantee correct genealogy. The system must prevent an operator from issuing an unapproved material, skipping a required verification, or completing a process step after a failed result without an authorized disposition.
Connect process equipment to quality records without mistaking data for control
Equipment connectivity is valuable when it captures evidence directly from the process and makes deviations visible while they can still be contained. It is less valuable when it merely creates a large archive of unreviewed machine signals. The first priority is to identify process conditions that can make a product nonconforming even when visual inspection passes.
Consider an ultrasonic cleaning stage before coating, bonding, welding, or assembly. The quality record may need to establish that the correct cleaning program was selected, that the part was processed for the required cycle, and that the cleaning medium was within its controlled condition. For a surface treatment or electrostatic coating process, coating thickness, surface preparation status, curing conditions, and grounding or application controls may be relevant depending on the specification. For vacuum systems supporting degassing, packaging, coating, freeze-drying, or semiconductor-related operations, the critical issue is often whether the required vacuum condition and process duration were achieved without an unresolved alarm.
These records should be linked to a product or batch identity at the time of processing. A machine historian may show that a chamber alarm occurred at 10:17, but that alone does not identify the products at risk. Conversely, a work order history may show that a batch used the chamber, but it may not reveal whether the chamber was operating within the required window. An effective industrial quality assurance system brings both pieces together.
There should also be a deliberate distinction between monitoring and acceptance. A sensor can show a trend; it does not automatically define a conforming product. Acceptance criteria need approved limits, a response rule, and ownership. When a reading moves outside a control range, the system should indicate whether the process must stop, whether material since the last verified good point must be placed on hold, and who can authorize further action. Without this decision logic, connected equipment can create confidence without improving control.
Build release gates around evidence, not assumptions
Traceability becomes operationally useful at release points. Incoming material release, batch release, final inspection, packaging verification, and shipment release should each depend on evidence appropriate to the risk. The evidence may include supplier documentation, receiving inspection, calibrated measurement results, process completion status, visual checks, code verification, or review of deviation records.
For quality teams, the most important design question is whether a product can move forward when required evidence is missing. In a mature system, the answer is controlled by the process rather than left to memory. A batch should not be released because its paperwork is expected to arrive later. A serialized product should not be dispatched if its permanent mark cannot be read or does not resolve to the correct production record. A coating lot should not be released merely because it looks acceptable when the required cure or thickness evidence is absent.
This does not require every release to be slow or paperwork-heavy. Automated checks can validate that required records exist, that a measurement was within the approved limit, that a material is not expired or blocked, and that equipment calibration status was valid at the time of use. Human review should remain focused on exceptions, complex deviations, and decisions requiring technical judgment.
Safety and compliance personnel should be included when defining release conditions. A quality disposition can have safety implications when contamination, material substitution, inadequate cleaning, incorrect formulation, incomplete marking, or surface-treatment failure could affect product use, handling, or regulatory obligations. The release workflow should therefore make it clear who owns the technical evaluation, who owns the safety assessment where applicable, and how the final decision is documented.
Design deviation handling before the first recall or complaint
The test of a traceability system is not whether it can generate a production report under normal conditions. The test is whether it can respond to an exception with a defined, credible scope. When an issue is detected, the team should be able to establish the last known good point, the first known affected point, the materials and products within that interval, the current locations of those products, and any customer shipments that may require action.
That requires disciplined treatment of alarms, failed inspections, calibration issues, and process interruptions. A deviation should not be closed simply because the equipment was restarted or the next unit passed inspection. The record needs to identify potentially affected material, the immediate containment action, the investigation route, the final disposition, and whether corrective action changes the approved process. Where an investigation cannot establish a precise boundary, the containment boundary should be conservative enough to protect product integrity.
Periodic trace exercises are useful because they expose errors that routine production hides. Select a finished lot or serialized unit and trace it backward to materials, process records, inspections, and equipment status. Then select an incoming material lot or a process event and trace it forward to finished goods and shipments. The exercise should measure whether the information is complete and usable, not merely whether records exist somewhere in the organization.
Use implementation stages that match operational maturity
A full digital traceability architecture may be justified for complex, regulated, high-volume, or multi-site production, but it is not the only route to better control. A practical implementation can begin with the operations that create the highest quality or safety exposure. For many facilities, those are material identity at receiving and issue, batch weighing, critical cleaning or treatment stages, permanent product coding, final release, and shipment linkage.
The first stage should establish standard identifiers, controlled labels, clear hold status, and a consistent event record. The second can connect selected equipment data and automate validation at release points. Later stages may integrate laboratory results, maintenance records, supplier quality data, and customer complaint analysis. This sequence is often more effective than attempting to digitize every form at once, because it forces the organization to prove that each new record supports a decision.
The system also needs ownership after launch. Quality can define acceptance requirements, but operations must follow the identity and handoff rules. Engineering must maintain parameter definitions and equipment interfaces. Information technology must protect record availability, access control, and change management. Compliance and safety teams must ensure that exceptions are assessed at the right level. Traceability deteriorates quickly when changes to labels, recipes, equipment programs, or routing are made without updating the corresponding quality controls.
A well-built industrial quality assurance system does not promise that defects will never occur. It gives the organization a disciplined way to prevent avoidable escapes, detect deviations earlier, limit the scope of affected product, and explain release decisions with evidence. For production environments where cleanliness, formulation accuracy, process stability, permanent identification, and surface performance all influence final quality, that evidence is part of the product itself.