
A traceable production line fails when the identifier cannot be read, cannot be trusted, or cannot be connected to the production record that explains it. The lowest machine quotation rarely captures those failure modes. A sound evaluation of a laser marking solutions supplier starts with the delivered marking result on the actual part, then moves outward to integration, data handling, validation, maintenance, and the cost of recovering from unreadable or mismatched codes.
Requesting a generic sample plate is a weak basis for comparison. The relevant evidence is a representative production sample: the same material grade, surface condition, geometry, coating state, expected code content, and post-process exposure. A dark mark on a flat anodized coupon says little about a small Data Matrix code on a curved stainless-steel component that will later be passivated, washed, assembled, and exposed to abrasion.
Start with the traceability requirement, not the laser source
Before comparing fiber, UV, green, or CO2 systems, define what the mark must prove and where it must remain readable. A serial number intended for visual identification has different requirements from a two-dimensional code used for automated genealogy, warranty control, anti-counterfeiting, or regulated product records. The mark needs a specified relationship to the part record: a unique identifier, a batch reference, a timestamp, process status, or a combination of those fields.
Code content directly affects cycle time and readability. More characters, tighter cell sizes, and higher error-correction settings increase the marking burden. A supplier that quotes a cycle time without stating code size, data string, marking field, part position, and verification method has not supplied a usable production figure. Ask for the complete code template and the intended scan distance, camera type, and lighting arrangement.
Traceability also has a temporal dimension. If a code is assigned before a critical process but the part is later rejected, the production system must preserve that event rather than leaving an apparently valid identifier attached to an invalid part. The marking station, supervisory controls, and quality record need a defined method for handling rejected, reworked, quarantined, and duplicate parts.
Evaluate permanence as a material-and-process result
“Permanent” is not a single mark characteristic. It describes how a particular mark survives the environment and downstream operations. A surface discoloration may be appropriate for a cosmetic label but disappear after cleaning. A deep engraving may survive abrasion yet create burrs, stress concentrators, or particle contamination on a precision component. Annealing on stainless steel can create a smooth dark contrast mark with minimal surface disruption, while ablation removes a coating to reveal a contrasting substrate. Each outcome needs to match the part’s functional limits.
Material condition deserves as much attention as material name. Stainless steel may be polished, bead-blasted, cast, oily, passivated, or coated. Aluminum may be bare, anodized, painted, or treated with conversion coatings. Plastics vary by pigment, filler, moisture condition, mold-release residue, and thermal sensitivity. Similar-looking marks can originate from different interactions with the substrate, so visual acceptance alone is insufficient.
Request trial samples that reflect realistic variation, including surface roughness ranges, lot-to-lot color changes, and component temperature at the station. Where parts arrive with oil, dust, fingerprints, or residual cleaning chemistry, establish whether pre-cleaning is required. A code that scans in a demonstration but becomes inconsistent after a wash, coating, heat cycle, or sterilization step should be treated as an unresolved process condition rather than a minor parameter adjustment.
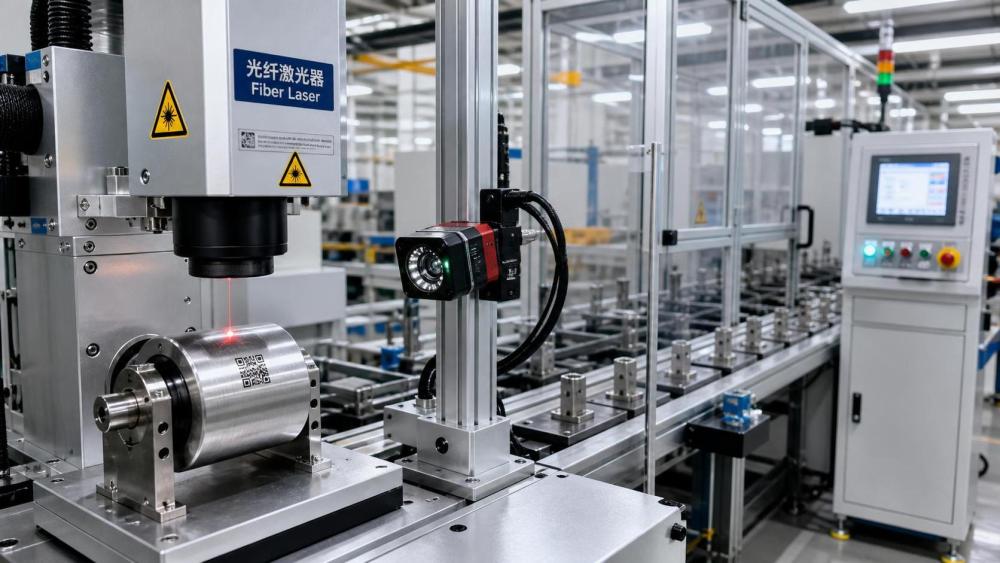
Durability testing should follow the actual exposure sequence. That may include solvent wiping, corrosion exposure, thermal cycling, vibration, abrasion, coating, or assembly contact. The relevant question is not whether a mark remains visible after one test, but whether code contrast, module integrity, and scan reliability remain within the agreed acceptance criteria after the part’s expected treatment. The supplier should be able to explain which laser parameters influence these outcomes: pulse energy, repetition rate, spot size, hatch spacing, focal position, passes, and marking speed.
Readability must be measured at the point of use
A readable code is not automatically a robust code. Handheld scanners, fixed readers, vision cameras, and mobile inspection devices have different optical limits. A code can pass with the supplier’s high-quality camera and fail at a line-side reader because the installed lens, working distance, illumination angle, motion blur, or part presentation is different.
Set the verification condition before ordering. It should identify the symbology, nominal code size, minimum quality grade or internal threshold, aperture or reader configuration where relevant, and the number of reads expected during normal production. The criteria should distinguish a code that is technically decodable from one that has sufficient margin for variation in focus, surface finish, and handling.
Focus control is often underestimated. Parts with height variation, curved surfaces, changing fixtures, or multiple marking faces may need autofocus, a controlled Z-axis, or a fixture that holds the marking surface at a repeatable focal plane. Adding motion hardware can improve consistency, but it also changes integration complexity, cycle time, and service exposure. The proposal should state which axes are included and which are assumed to be supplied elsewhere.
Compare the complete station boundary
A laser head alone is rarely the operating solution. A credible quotation identifies the boundary between supplied equipment and line responsibilities. That boundary may include the laser source, marking head, controller, safety enclosure, part fixture, rotary axis, conveyor interface, fume extraction connection, vision verification, barcode reader, stack light, electrical cabinet, and controls programming. Ambiguity at this stage often appears later as unbudgeted fabrication, delayed commissioning, or an interface that cannot meet the intended cycle time.
Part handling needs particular scrutiny. A marking cell may achieve excellent beam-on speed while the total station time is constrained by loading, clamping, scanning, fixture indexing, guarding, and release. Ask for a time breakdown that separates data receipt, part detection, positioning, marking, verification, pass/fail decision, and handoff. This reveals whether the proposed system has margin for normal line variation or only works under ideal demonstrations.
Safety design should be evaluated as an installed condition, not as a component label. Confirm enclosure access points, interlocks, viewing windows, door logic, emergency stop interfaces, maintenance access, and the treatment of open loading zones. If the mark generates plume, residue, or odor, determine the extraction requirement and whether the extraction system, duct connection, filters, and monitoring are inside the scope. Poor fume control can contaminate optics, degrade mark quality, and increase cleaning frequency.
Data connectivity is part of marking quality
Traceable marking depends on correct data at the correct part. The interface must specify how the station receives the identifier, how it acknowledges completion, and what occurs when communication is interrupted. A simple start signal and a local serial-number counter may suit isolated work, but it creates obvious duplication and recovery risks in a connected line.
Clarify the source of truth for serial numbers. The station should not silently generate a new code after an interrupted cycle unless the production record and physical part status are reconciled. Define the behavior for a failed verification read, a part removed before completion, a restarted controller, an operator retry, and a rejected mark. Those conditions are where duplicate identities and orphan records are created.
Supplier documentation should describe the protocol, field definitions, message timing, error codes, and data retention available at the station. It should also state whether code content is locked by recipe, editable locally, or supplied externally. Local editing may be useful during setup, yet unrestricted changes can undermine traceability. A controlled recipe structure with logged changes is easier to validate than an informal set of manually adjusted parameters.
Use acceptance testing to expose commercial assumptions
Factory acceptance should prove more than that the equipment powers on and creates a visible mark. The test should use agreed representative parts and include normal production code content, specified placement tolerances, target cycle time, verification results, interface signals, reject responses, and safety functions. Site acceptance should repeat the conditions that depend on the real installation: utilities, extraction, line controls, material flow, reader optics, and downstream treatment.
Acceptance criteria need a defined response when results fall short. A vague promise to “optimize parameters” leaves responsibility unclear when the part surface varies or a reader fails. Establish whether corrective work includes fixture revision, software changes, optical adjustment, additional trials, or only remote parameter guidance. The distinction matters because a marking issue can originate in the supplied equipment, the incoming part, the plant environment, or the integration design.
Ask for the parameters, recipes, drawings, electrical documentation, software backup procedure, and revision history needed to restore the station after a controller replacement or line upgrade. Ownership and access to these materials affect the practical cost of long-term operation. A system that cannot be restored without a specialist visit creates avoidable downtime exposure.
Calculate cost through the operating life
Capital price should be compared with the installed and operating scope. Include enclosure and guarding work, fixtures, motion equipment, vision verification, extraction, controls integration, installation, site commissioning, training, spare parts, and periodic optical maintenance. A lower initial quote may exclude the elements required to achieve a stable traceable process.
Service capability is best assessed through specifics: response pathway, remote diagnostic access, availability of critical modules, local or regional technical coverage, expected maintenance tasks, and lead time for replacement optics, controllers, and laser-source components. Request a clear description of consumables and wear items. Laser marking itself may use no ink, but filters, protective windows, extraction components, fixtures, and vision lighting still require attention.
Finally, assess whether the proposed architecture can accommodate foreseeable variation without replacing the entire station. A new code format, an additional part family, a changed coating, or a different reader may require unused controller capacity, adjustable tooling, larger marking fields, software configuration, or process revalidation. The appropriate level of flexibility is defined by the production roadmap, not by a generic claim that a system is “future-proof.” The preferred supplier is the one that demonstrates the required mark, proves the data path, defines responsibility at each interface, and documents the conditions under which performance remains repeatable.