
Traceability marking is not the same as putting readable text on a part
That distinction is where many evaluations of laser marking systems USA buyers review begin to go wrong. In regulated production, a mark is not judged only by how sharp it looks when the sample leaves the machine. It is judged by whether the code still links the product to its batch, process history, operator actions, inspection records, and shipping documentation after cleaning, handling, sterilization, coating, transport, or years of field use. A visually clean logo or serial number may still fail the real traceability requirement if it cannot be scanned consistently, if it distorts the substrate, or if it cannot be validated within the manufacturer’s quality system.
This matters in U.S. supply chains because traceability is often driven by a combination of sector-specific rules, customer specifications, internal quality procedures, and audit expectations rather than one single “laser marking law.” Medical device manufacturers may need direct part marking that remains legible after sterilization and use. Aerospace suppliers may work to UID or customer-imposed 2D code requirements. Automotive and electronics producers may be pushed by warranty analysis, recall containment, and anti-mix controls. In each case, the marking system becomes part of the evidence chain.
What quality and safety teams should actually evaluate
A useful evaluation starts with the traceability objective, not the laser source. The first question is simple: what must the mark prove, and under what conditions must it remain readable? That answer affects everything else, including wavelength choice, marking method, vision verification, software controls, and validation burden.
For regulated applications, five criteria usually matter more than brochure-level power ratings.
- Permanence under actual exposure: abrasion, solvents, passivation, heat, sterilization, UV, or outdoor service.
- Data integrity: the right code, linked to the right record, generated without formatting or serialization errors.
- Material compatibility: no unacceptable cracking, melting, corrosion initiation, coating failure, or surface damage.
- Readability and verification: the code must be measurable, not just subjectively “easy to read.”
- Control and auditability: user access, change control, recipe management, and event logging must fit the plant’s quality system.
That is why two systems that produce similar-looking samples in a demo room can perform very differently once they are integrated into a validated production environment.
The compliance question is rarely only about the machine
Teams often ask whether a laser marker is “compliant.” The better question is whether the full marking process can be shown to support compliance. The machine is only one element. The process also includes the code content, data source, marking location, fixturing, operator permissions, inspection method, rejection logic, and record retention. In some industries, software behavior matters as much as beam quality. If an operator can overwrite a lot number without trace, or if the interface allows uncontrolled template edits, the traceability risk remains high even if the mark itself is permanent.
For U.S. buyers, this is especially relevant when equipment is sourced globally. A technically capable system may still create headaches if documentation is thin, validation support is weak, service response is slow, or software records are not aligned with internal QA expectations. Safety and quality teams usually need more than a sample coupon; they need installation documentation, user access structure, preventive maintenance guidance, calibration or verification procedures where applicable, and a realistic plan for process qualification.
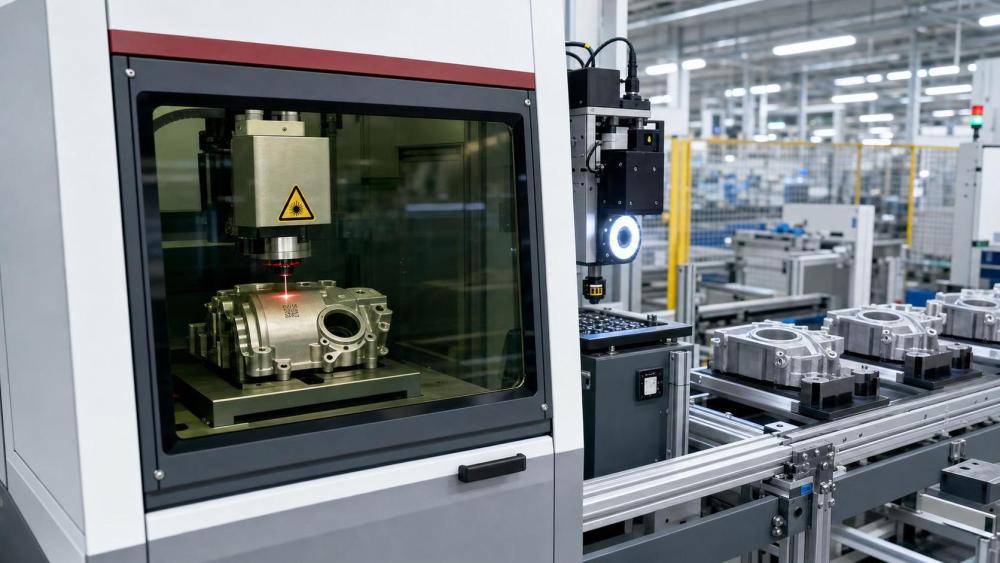
Choosing the laser source is a materials decision before it is a branding decision
A common mistake is to compare fiber, CO2, UV, and green lasers as if they were interchangeable tools with different price points. In practice, the material and the required mark behavior decide the shortlist. Metals often favor fiber systems for annealing, engraving, or high-contrast marking, but the exact result depends on alloy, finish, oxide condition, and required depth. Plastics can be more complicated. Some resins respond well, some discolor unpredictably, and some require additives for reliable contrast. Coated surfaces may produce excellent visual marks while hiding adhesion loss or heat-affected damage underneath.
For compliance-driven traceability, “best contrast” is not always the right target. On stainless components, for example, a deep mark may seem safer than a dark annealed mark, yet the process requirement might actually favor minimal surface disruption if corrosion behavior or cleanability is critical. On medical plastics or electronics housings, a strong visible mark may come at the cost of microcracking, particulate generation, or cosmetic rejection. Evaluation should therefore include not just legibility, but the effect of the mark on the part’s intended function and post-process environment.
Readable to the eye is not the same as verifiable
Where traceability relies on Data Matrix or other machine-readable codes, verification should be part of the conversation from the beginning. Many disputes arise because a code appears acceptable during setup but performs poorly in the field due to low cell contrast, poor quiet zone control, surface curvature, glare, or inconsistent dot geometry. Human-readable text can mask those weaknesses for a long time.
This is why regulated manufacturers often pair the marking unit with vision inspection or code verification rather than relying on operator judgment alone. The exact grading method depends on the application and customer requirement, but the principle is consistent: define a measurable acceptance threshold, then prove the process stays inside it over time. That means testing across normal production variation, not only on one ideal substrate from the lab bench.
Integration risk often shows up later than marking risk
On paper, a standalone marking head may look easy to approve. In production, the harder issues tend to involve integration. Can the system receive the correct data from MES, ERP, PLC, or vision stations without manual re-entry? Does it prevent duplicate serial numbers? What happens after a stop, a rejected part, or a rework event? Can the line prove which code was marked on which part at which time? Those questions belong to quality engineering, not just automation.
For safety managers, enclosure design and operator protection are part of the same evaluation. U.S. facilities generally need to consider laser safety classification, guarding, interlocks, fume extraction, and maintenance access. A system that delivers an excellent mark but creates uncontrolled fumes, poor access for cleaning, or risky bypass behavior is not well specified for a regulated plant. The right supplier should be able to discuss both marking outcomes and the controls needed around them.
What buyers in the USA should expect from suppliers
When reviewing laser marking systems USA manufacturers and integrators provide, quality teams should expect evidence of process understanding, not just machine availability. A credible supplier usually asks for substrate details, finish condition, downstream exposure, code format, cycle time, and inspection criteria before recommending a configuration. If the discussion stays at wattage, speed, and price, the evaluation is probably still too shallow for regulated traceability work.
They should also be prepared to support trials that reflect production reality: actual parts, actual cleaning chemistry if relevant, actual coatings, and realistic sample volumes. Short sample runs are useful, but they do not replace a disciplined process window study. In many plants, the winning system is not the one that makes the darkest mark. It is the one that keeps code quality stable across lot variation, shift variation, and routine maintenance intervals.
The most expensive failure is usually not a bad mark, but a weak traceability system
There is a practical lesson behind most marking-related nonconformities: traceability fails at the system level. The root cause may be poor contrast, but it may also be wrong data mapping, unverified code structure, uncontrolled template edits, untested durability, or line integration that cannot reconcile rejects and reprints. That is why evaluation should be led by the record the mark must support, then worked backward to the laser, optics, software, and controls.
For teams responsible for audit readiness, the most useful buying question is not “Which laser marker is best?” It is “Which marking process can we defend, repeat, and verify under our own regulated conditions?” Once that question is answered clearly, supplier comparison becomes much more rigorous, and much less vulnerable to attractive but incomplete demos.