
Start with the part, not the laser
When teams evaluate laser marking for metal parts, the first mistake is usually the same: they begin by comparing laser models before they have pinned down what the mark has to survive, how fast the line runs, and what the code is supposed to prove later. A clean-looking sample on a bench means very little if the part will later see oil, passivation, blasting, heat, solvent cleaning, or scanner-based traceability checks.
A better way to choose laser marking for metal is to work through the decision in the same order production will feel the consequences: material, surface condition, mark content, cycle time, verification, and maintenance reality. That sequence tends to expose weak assumptions early, before you end up buying a system that marks nicely in trials but struggles in actual production.
Check the base metal and the surface condition together
Do not treat “metal” as one category. Stainless steel, aluminum, carbon steel, plated steel, titanium, brass, and coated parts respond differently, and sometimes the coating matters more than the substrate. The same laser that produces a crisp dark mark on stainless may create low contrast on raw aluminum or damage a thin plated layer if the process window is tight.
Before you compare equipment, build a short material checklist:
- Base alloy or metal grade
- Surface finish: machined, polished, bead blasted, brushed, cast, anodized, coated, plated
- Part color and reflectivity
- Any pre-treatment or post-treatment after marking
- Whether the mark must change color, remove coating, anneal the surface, or engrave into the part
This is where many selections go off track. A supplier may show a sharp code on a flat stainless coupon, while your actual part is curved, oily, and zinc-plated. Those are not small details. They change contrast, focus tolerance, and the risk of damaging a functional surface.
Decide what kind of mark you really need
“Permanent” is too vague to be useful. In practice, most technical evaluations come down to four mark types, and each pushes the laser choice in a different direction.
If the part carries a serial number for internal routing only, a visible surface mark may be enough. If the code is there for lifetime traceability, counterfeit resistance, or downstream warranty analysis, the mark has to hold up after handling, assembly, and field exposure. That usually changes the process target immediately.
Match the laser process to production speed before you ask for cosmetic perfection
A lot of evaluation teams over-focus on the best-looking mark and under-focus on the acceptable mark at line speed. The real question is not whether a system can produce an excellent code in a lab. It is whether it can produce a readable, compliant, repeatable code within your available cycle time.
Use these checks during selection:
- Measure actual time budget per part, including loading, positioning, triggering, marking, and verification.
- Separate fixed content from variable content. A static logo and a changing 2D code do not consume time in the same way.
- Ask whether the line runs one-up or marks multiple parts per cycle.
- Check whether deeper engraving is truly required or whether a durable surface mark will satisfy traceability needs.
Here is the tradeoff people learn the hard way: when you ask for more contrast, more depth, larger data content, and tighter code quality at the same time, throughput usually becomes the constraint. A realistic selection process forces those priorities into the open.
Define traceability by reading method, not by label
If someone says the part needs “traceability,” stop and unpack it. Traceability can mean a human-readable lot code, a machine-readable serial number, a Data Matrix code linked to manufacturing records, or a UID-style identifier used across logistics and service systems. Those are different jobs.
For each part family, define:
- What data must be marked
- How that data will be read: operator, handheld scanner, fixed camera, customer inspection, field service
- At what stage it must remain readable
- Which system owns the code content and serialization logic
This matters because code quality is not judged by appearance alone. A mark can look dark and sharp but still fail if cell geometry, quiet zone, distortion, or part curvature interferes with scanning. Technical evaluators should request sample validation under the same reading method the factory will actually use, not just a photograph of the mark.
Look closely at part geometry and fixturing
Flat sample plates hide a lot of problems. Real parts rotate, vary in height, and present awkward surfaces. Small cylindrical parts, cast housings, fasteners, and polished components each create different alignment and focus challenges. If the fixturing concept is weak, even a capable laser process will behave inconsistently.
Check these points early:
- Part-to-part position tolerance at the marking station
- Whether the code area is flat, curved, recessed, or interrupted by features
- Required focal tolerance across the marking field
- How the system confirms part presence and orientation
A common miss is approving a process on one ideal fixture, then discovering later that upstream handling variation shifts the mark location enough to affect readability. If your line has multiple part variants, include the worst-case geometry in the trial set. That tells you much more than the easiest sample ever will.
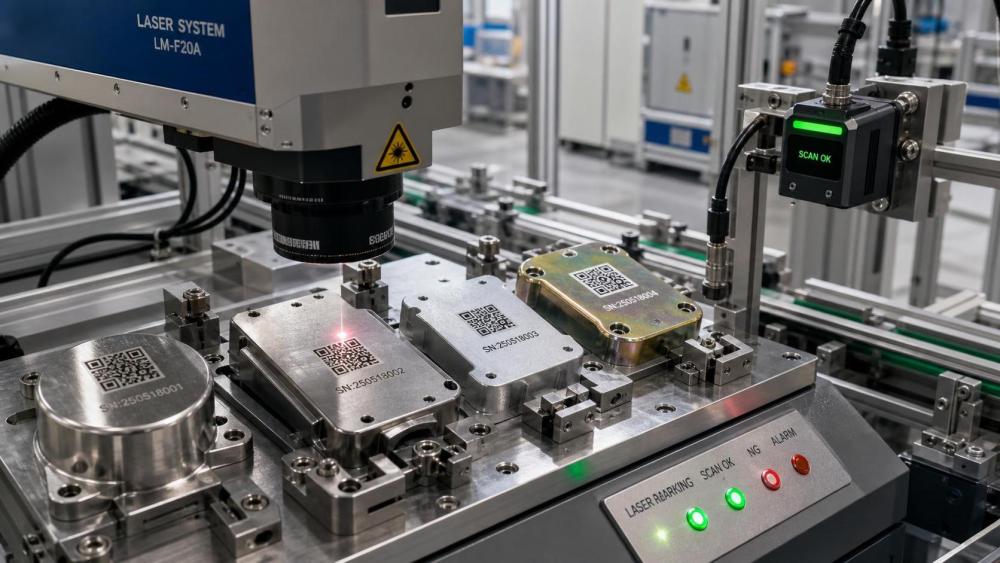
Do not separate marking from verification
For serialized metal parts, marking and checking are part of the same process. If the station marks a code but does not confirm readability before the part moves on, the hidden scrap cost can be much higher than the marking cost itself. Rework is also harder once the part has gone through coating, assembly, or packaging.
During evaluation, ask where verification sits:
- Integrated immediately after marking
- At a separate vision station
- Only by periodic operator checks
The last option is usually where traceability discipline starts to drift. If the code matters for recall control, process genealogy, or export documentation, define pass-fail rules before the equipment trial. Otherwise everyone says the sample “looks fine,” and nobody agrees later on what failure actually means.
Check what happens before and after marking
The mark is only one step in the route. Upstream oil, coolant residue, oxidation, or inconsistent blasting can destabilize contrast. Downstream washing, passivation, painting, plating, or heat treatment can reduce readability or change the surface around the code enough to confuse scanners.
When comparing options, ask a practical question: at which process step should the part be marked so the code remains useful without creating extra handling? Sometimes the best answer is not “as early as possible.” Mark too early, and later processing may compromise the code. Mark too late, and you lose in-process traceability where it may be most valuable.
Be specific about what the supplier has to prove in trials
A vague sample request produces vague results. Send real production parts, with realistic surface condition, and define the evaluation criteria in writing. That should include the code type, content length, target location, cycle time, expected readability method, and any downstream exposure the mark must survive.
Good trial questions are usually simple:
- Can the system achieve required readability on the worst surface, not just the best one?
- Does mark quality hold across the full batch, or only on selected pieces?
- What process margin exists if the part finish shifts slightly?
- What operator adjustments are needed between variants?
This is also where technical evaluators should watch for over-tuning. If a supplier needs extensive manual adjustment to make one sample set pass, that may be a warning sign for production stability.
Do not ignore maintenance, extraction, and software workflow
The laser source gets most of the attention, but day-to-day usability often depends on less glamorous items: fume extraction, lens cleanliness, recipe control, user permissions, code data handling, and integration with MES or ERP workflows where required. A technically sound marking process can still become a production nuisance if setup control is loose or maintenance access is poor.
Ask who will own template changes, serialization rules, backup, and job release control. If multiple plants or shifts will run the same part family, recipe discipline matters almost as much as laser performance.
A practical selection order that works
If you need a clean decision path, use this order. It keeps the conversation tied to production reality instead of brochure language.
- List part materials and actual surface states.
- Define whether the mark must be visible, scannable, deep, or resistant to later processing.
- Set the real cycle time and part-handling conditions.
- Specify data content and the exact reading method.
- Trial the hardest parts, not the easiest ones.
- Verify readability after the downstream steps that matter.
- Compare maintenance and control workflow before final selection.
That sequence tends to expose whether you need a fast surface mark, a more robust engraved code, a process tuned for coated metal, or a station built around verification discipline. It also helps separate nice-to-have cosmetic preferences from the requirements that actually protect throughput and traceability.
In most projects, the right laser marking choice for metal parts is the one that stays readable where your process is least forgiving: the roughest surface, the shortest cycle, the most demanding code, or the harshest downstream treatment. If you evaluate against that condition first, the final equipment decision usually becomes much clearer.