
Choosing Anti-Counterfeit Product Marking for Durable, Verifiable Traceability
Anti-counterfeit product marking is often treated as a printing or labeling decision. In practice, it is a traceability decision with consequences for quality control, warranty handling, regulatory evidence, export documentation, and field-service work. A code that looks clear when it leaves the factory but fades after heat exposure, chemical washing, abrasion, or outdoor storage is not a durable identifier. It is a future investigation waiting to happen.
For technical evaluators, the central question is not simply whether a laser marker or industrial inkjet printer can place a serial number on a product. The real question is whether the marking method remains readable, difficult to alter, connected to a reliable data record, and practical within the actual production process. These requirements do not always point to the same technology.
A robust selection begins with the product’s full life cycle: what the item is made of, where the mark will be placed, how it will be handled, which environments it will encounter, who must verify it, and what happens when a code cannot be read. This is especially relevant in advanced manufacturing, where cleaning quality, surface condition, coating processes, vacuum handling, and production consistency can all affect the final appearance and legibility of a mark.
Start with the threat model, not the marking machine
“Anti-counterfeit” covers several different risks. Unauthorized copying is one. Diversion into unauthorized markets, relabeling of lower-grade products, replacement of service parts, warranty fraud, and alteration of expiration or batch information are others. A simple human-readable lot code may be adequate for internal process control, yet offer little resistance against deliberate copying. Conversely, a highly sophisticated security feature may add cost without solving a basic issue such as poor serial-number governance.
It helps to separate marking into three layers. The first is identification: part number, batch, date, serial number, or machine-readable code. The second is verification: a person, scanner, vision system, distributor, or customer can confirm that the identifier exists and is valid. The third is resistance to manipulation: removing, overwriting, transferring, or reproducing the mark becomes more difficult or more evident.
No marking method is counterfeit-proof in isolation. A permanent laser-etched Data Matrix code can still be copied visually if the same data can be duplicated. A serialized code with cloud-based authentication can still fail if access rights, duplicate scans, and returned-product procedures are poorly managed. The equipment choice therefore needs to sit inside a broader control plan covering serialization, data generation, verification, exception handling, and retention of production records.
Durability is a product-and-process question
A mark should be specified against the conditions it must survive, not against a vague expectation of permanence. Technical teams should map exposure before comparing suppliers. Typical factors include abrasion during assembly, solvents used in cleaning, heat cycling, UV exposure, humidity, salt-containing environments, oils, curing ovens, sterilization, and repeated contact with operators or scanning fixtures.
Substrate condition matters as much as substrate type. Stainless steel, anodized aluminum, bare aluminum, coated metal, molded plastic, rubber, glass, ceramic, cardboard, flexible film, and painted surfaces all respond differently. Even two parts made from the same nominal material can behave differently when one has residual oil, mold-release residue, oxide scale, a textured finish, or a conversion coating.
This is where auxiliary manufacturing systems become part of the marking decision. A component leaving ultrasonic cleaning with residual contamination may produce inconsistent laser contrast or poor ink adhesion. A coated enclosure marked before curing may not represent the final surface condition. Vacuum-related packaging processes can impose environmental demands that are not obvious when the coding equipment is evaluated on a bench. The marking station should be assessed as part of the process chain rather than as a standalone add-on.
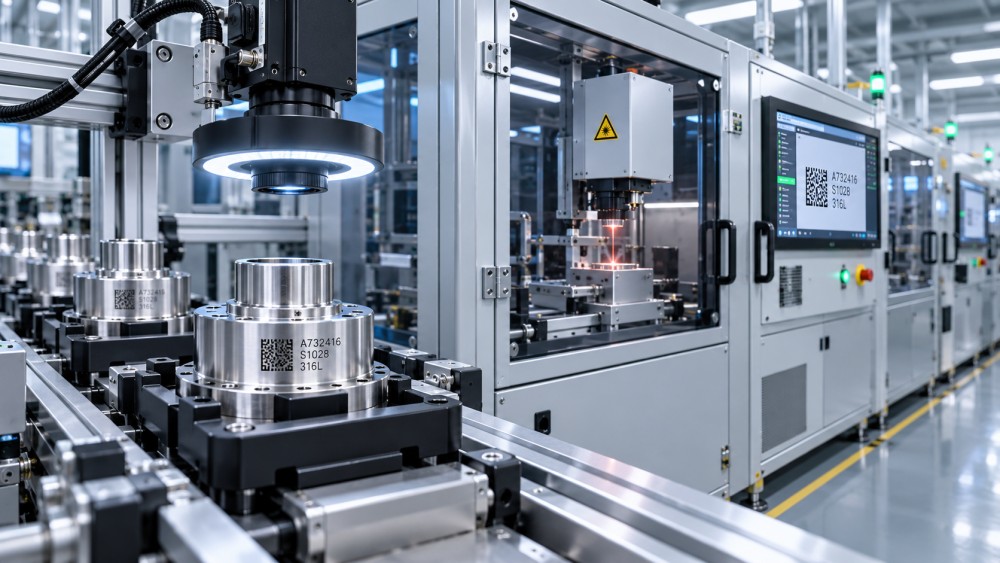
Durability testing should reflect the actual application. It is tempting to approve a sample based on an attractive first impression, particularly with high-contrast laser marks. But contrast, adhesion, depth, readability, and surrounding surface damage are separate properties. A dark mark may be readable but too shallow to withstand abrasion. A deep engraving may survive harsh handling but create stress concerns in thin-walled or fatigue-sensitive parts. On some plastics, aggressive laser settings can create brittleness, discoloration, fumes, or a rough surface that collects contamination.
Laser marking and inkjet coding solve different problems
Laser marking is frequently selected where permanent identification is required on metal, engineering plastics, coated components, tools, medical-device components, electrical parts, and durable industrial assemblies. Depending on the material and laser type, it may create annealed contrast, color change, foaming, ablation, or engraving. Its strengths are the absence of consumable ink, strong integration potential, and the possibility of high-resolution machine-readable codes on many rigid substrates.
Its limitations are equally practical. Laser interaction is material-specific; a configuration that performs well on one polymer grade may not work on another. Reflective, curved, heat-sensitive, or uneven parts need careful fixturing and process development. Fume extraction, guarding, interlocks, lens cleanliness, focus management, and part presentation are not minor installation details. They influence uptime and mark consistency.
Industrial inkjet coding is often more flexible for high-speed packaging lines, cartons, bottles, films, cables, coated surfaces, and products where non-contact variable-data printing is needed. It can be a sensible choice when production formats change frequently or the marking area is not fixed. Yet ink selection, drying time, adhesion, printhead maintenance, environmental cleanliness, and substrate variability must be evaluated honestly. Inkjet can provide effective traceability, but it is not automatically the right choice when the code must remain legible after aggressive chemical exposure or years of outdoor service.
Many plants use both. A durable direct mark can identify the product itself, while an inkjet code on outer packaging supports logistics, batch handling, or market-specific labeling. Treating these as competing technologies can obscure a more reliable layered design.
Readability must be designed, then verified
A serial number visible to the human eye is not necessarily machine-readable. A 2D symbol may scan successfully with one handheld reader but fail on the vision system used downstream. Code size, cell geometry, print or mark contrast, quiet zones, curvature, lighting, viewing angle, and the scanner itself all influence performance. Where customers, regulators, distributors, or internal automated systems require a specific symbology or grading method, those requirements should be confirmed before selecting the marking cell.
The difficult production question is not “Can the code be read?” but “How will unreadable codes be detected without slowing the line or releasing unverified parts?” For high-consequence items, an inline vision check linked to reject handling may be justified. For lower-volume industrial assemblies, controlled offline verification may be sufficient. The appropriate level depends on the cost of a missed defect, the likelihood of manual handling errors, and the ability to quarantine suspect products.
Verification logic should include more than presence. A system may confirm that a mark exists while failing to detect an incorrect serial number, a duplicate record, an improperly formatted batch code, or a code written to the wrong product variant. The marking equipment, manufacturing execution system, database, and inspection process should use a clear handoff: generate data, mark it, read it back, compare it with the expected record, and log the result. If this chain is fragmented, traceability becomes difficult to defend later.
Avoid the common selection shortcuts
One common shortcut is choosing the deepest possible mark because it appears most permanent. Deep engraving can be appropriate, but it may be unnecessary for products with modest exposure and may affect appearance, cleaning, coating, or mechanical integrity. Another is selecting a code size based solely on available space. A code that technically fits may leave too little tolerance for process variation, surface texture, or scanning distance.
A third mistake is validating only pristine samples. Production parts arrive with realistic variation: different lots of material, small shifts in color, wear on fixtures, dust, residual moisture, changing line speed, and operator intervention. A meaningful trial uses representative parts and realistic upstream conditions. It should also test rework rules. If a mark is unreadable, can the part be re-marked? If so, where, how is the original data controlled, and can the rework itself create ambiguity?
Technical evaluators should also ask where the code will be read after shipment. A perfectly marked identifier has limited anti-counterfeit value if a field technician lacks the reader, a distributor cannot access the verification portal, or the product is commonly installed in a location that hides the mark. Verification must be usable by the people expected to perform it.
Build the evaluation around representative trials
The most useful supplier discussion is usually a sample-based process review rather than a feature comparison. Provide representative materials, surface finishes, part drawings, intended code content, expected cycle time, available marking area, and known exposure conditions. If the product will later be cleaned, coated, assembled, sterilized, or packed under vacuum, include that sequence. The goal is to determine not only whether a mark can be made, but whether it remains functional after everything else done to the product.
A practical acceptance plan normally defines the readable data, minimum visual and machine-reading expectations, inspection location, sampling or inline verification approach, response to failure, and records to retain. Exact acceptance criteria will vary by product, market, contractual requirements, and any applicable industry rules. They should not be copied blindly from another factory or product family.
For organizations comparing industrial auxiliary systems across multiple processes, marking should be reviewed alongside cleaning, surface treatment, coating, handling, and data capture. The final product may look like the output of a primary machine, but its identity and traceability often depend on these supporting processes being stable and connected.
Choose the control system, not just the mark
The right anti-counterfeit product marking solution is the one that matches the substrate, survives the real service environment, produces reliably readable data, and fits a disciplined verification workflow. Laser marking may be the stronger route for permanent direct part identification. Industrial inkjet may be the more practical option for fast, flexible coding on packaging or changing product formats. In many operations, the dependable answer is a deliberate combination of both.
Before approving equipment, ask one final operational question: if a disputed product appears in the field two years from now, can the organization read the mark, verify its data, understand its production history, and identify whether it has been altered? If the answer is uncertain, the gap is rarely solved by a more attractive code alone.